Waterjet Feed Rate Calculator
Estimate abrasive waterjet traverse speed from material, thickness, pressure, abrasive flow, orifice size, mixing tube, quality level, kerf, pierce time, and cut length.
Waterjet Cutting Results
| Material | Baseline Q3 Feed | Thickness Exponent | Cutting Note |
|---|---|---|---|
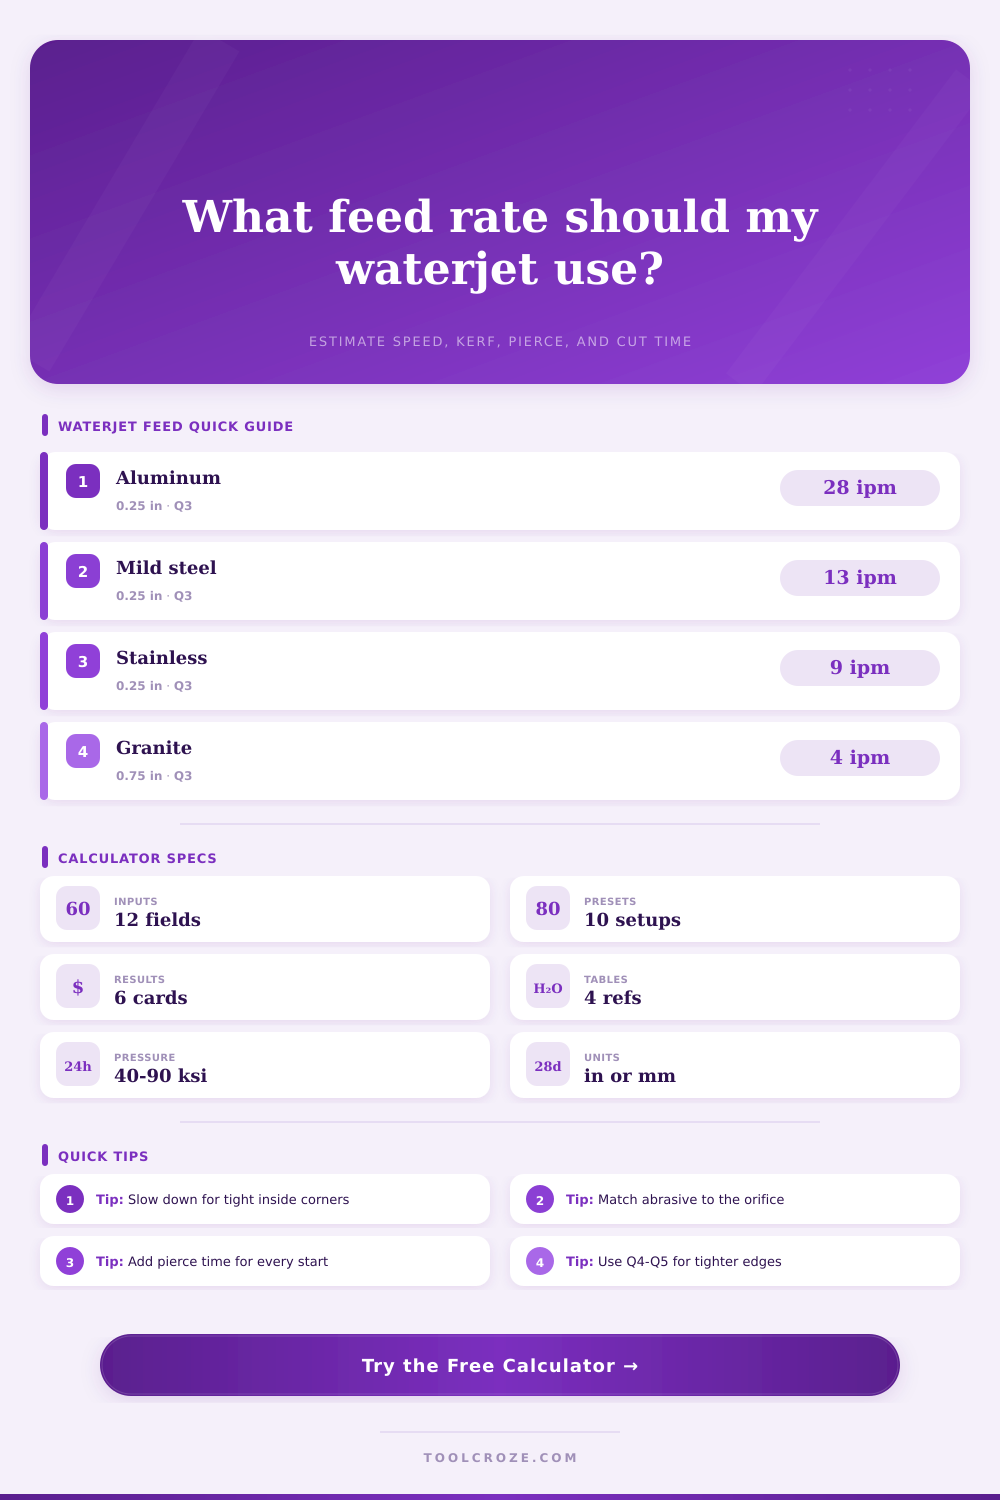
| Aluminum plate | 28 in/min at 0.25 in | 1.10 | Fast cutting with good abrasive coupling |
| Mild steel | 13 in/min at 0.25 in | 1.22 | General benchmark for abrasive waterjet cutting |
| Stainless steel | 9 in/min at 0.25 in | 1.28 | Slower edge speed for hard, tough alloy |
| Titanium alloy | 8 in/min at 0.25 in | 1.32 | Watch taper and use stable pierce settings |
| Copper or brass | 15 in/min at 0.25 in | 1.18 | Dense but generally cuts cleanly |
| Glass or tile | 18 in/min at 0.25 in | 1.05 | Use gentle pierce and controlled acceleration |
| Granite or stone | 11 in/min at 0.25 in | 1.16 | Brittle aggregate benefits from slower quality cuts |
| Carbon fiber laminate | 22 in/min at 0.25 in | 1.08 | Abrasive cuts reduce heat but edges still need support |
| Rubber or foam | 55 in/min at 0.25 in | 0.90 | Often cut with lower abrasive or water-only settings |
| Acrylic or plastic | 32 in/min at 0.25 in | 1.00 | Keep feed smooth to avoid edge chatter |
| Quality | Feed Multiplier | Typical Edge | Best Use |
|---|---|---|---|
| Q1 rough separation | 1.65x | Noticeable striation and taper | Scrap separation or rough blanks |
| Q2 rough production | 1.28x | Moderate striation | Parts with secondary finishing |
| Q3 general purpose | 1.00x | Balanced edge quality | General profile cutting |
| Q4 clean edge | 0.72x | Cleaner wall and lower taper | Visible edges and tighter fit |
| Q5 fine edge | 0.48x | Slowest, finest wall | Precision features and minimal finishing |
| Orifice | Mixing Tube | Typical Abrasive | Common Use |
|---|---|---|---|
| 0.010 in | 0.021-0.030 in | 0.45-0.65 lb/min | Fine features and thin stock |
| 0.012 in | 0.030-0.035 in | 0.60-0.85 lb/min | General shop cutting |
| 0.014 in | 0.030-0.040 in | 0.80-1.05 lb/min | Balanced speed and edge quality |
| 0.016 in | 0.040-0.045 in | 1.00-1.25 lb/min | Higher productivity cutting |
| 0.018 in | 0.045-0.050 in | 1.20-1.50 lb/min | Thick plate and high horsepower systems |
| Material Group | Thin Stock | Medium Stock | Thick Stock |
|---|---|---|---|
| Aluminum and copper | 1-4 sec | 4-10 sec | 10-25 sec |
| Mild steel and stainless | 2-6 sec | 8-20 sec | 20-60 sec |
| Titanium and hard alloys | 3-8 sec | 12-28 sec | 30-75 sec |
| Glass, ceramic, stone | 4-12 sec | 12-35 sec | 35-90 sec |
| Rubber, foam, plastic | 0.5-3 sec | 2-8 sec | 8-20 sec |
The steel needs cutting. There’s a deadline for turning in your quote by lunchtime, but the machine is already humming in the corner. No problem with the waterjet. It’ll cut steel. But will it cut fast enough that you’re making money? And will it do so cleanly enough to pass inspection?
All of these factor comes together at feed rate. For each job, it’s the single most important number you dial into the computer. Dial it correctly, and the machine purrs along. Dial it incorretly, and you waste garnet without purpose. This page’s tool will estimate it for you.
How to Calculate Feed Rate
To really operate well, however, you’ve got to know what inputs are. Now let’s begin with the material. Everything starts with the material. Titanium takes more time and more patience then aluminum. It go slower. And the calculator has baseline speed figures for each metal. Those speeds is also adjusted according to thickness.
The thicker the stock, the slower the cut will be, but not necessarily linearly. This is where the exponent comes into play. Cutting one-tenth of an inch deeper into a three-inch plate takes far longer then cutting that same tenth of an inch higher up in the stack. The stream weakens. The abrasive particles spread out. The intensity diminishes. So why does this mean we can’t simply use thickness ratios as multipliers of thin-stock speeds? Because the physics don’t allows it.
Next is the quality level. Here’s where most operator tweak their settings unwittingly and pay for it. Switching to a finer edge finish sounds like a no-brainer, right? Wrong. It’ll cut your feed rate by half. Go from a general purpose setting down to a fine edge finish and your feed rate will be halved. Sure, your wall is cleaner, but you doubled your cut time and your abrasive consumption. That’s a pretty steep trade off. And if the part is tucked away somewhere inside some assembly, then who cares about a mirror finish? These multipliers is clear in reference tables on this page. They’re not guesses; they impact your bottom line.
And don’t neglect pierce time. Many times pierce time will eat away at your shift more than the cutting itself in a nested job with lots of little hole. You have to enter number of pierces needed into the calculator and how long each one takes on average. Rushing through the pierce on heavy steel results in creating a crater. This then makes the jet has to work extra hard right out of the gate, ruining the initial few inches of the cut. On the other hand, waiting too long wastes seconds and adds up to minutes. It’s a fine balance based off material thickness and type, but over time you’ll get a good idea of what works best for your specific machine.
There’s also the hidden cost of kerf loss. Kerf is something you don’t really consider till you’re trying to meet a tight tolerance or fit it into a slot. That is the amount of volume you remove. You can use the calculator to see how much material becomes slurry. Seems small, but if you’re doing some precision work and overlook the kerf width you’ll have scrapped parts. This ties in to the mixing tube diameter input and orifice size input as well. The bigger the orifice, the more water/abrasive goes through, so it helps when working thicker sections, but it also increases the kerf width. A smaller hole reduces the stream but limits top speeds. Match nozzle to the job.
Finally, there is the machine efficiency factor. A perfect straight line is not how we cut in real life. Tight corners, acceleration, and deceleration reduces the average speed from the theoretical maximum. Even with the best controller there are physical limitations which means you have to factor in the gantry’s inertia. That’s what the percentage on the calculator is for.
Enter your numbers. Select your material. Your thickness. Your quality. Let it crunch the numbers. Voila: It suggests a feed rate. It provides an estimated total time. It indicates how much abrasive to expect to go through.
It is not a law. It is more like a good place to start. Quote confidently using this tool. Catch jobs that aren’t going to make you money. And know that sometimes the quickest cut isn’t always the best cut. Sometimes it’s the cut that gets done on time and clean. It also leaves some garnet in the bin for the next piece.