Skew-T Fillet Weld Calculator
Estimate skewed T-joint fillet weld geometry from included angle, unequal leg sizes, root opening, weld length, load direction, electrode strength, and correction factors.
📌Skew Joint Presets
⚙Weld Geometry Inputs
Skew-T Fillet Weld Results
🧱Weld Geometry Grid
📐Skew Angle Geometry Reference
| Included angle | Equal-leg throat factor | Geometry behavior | Field note |
|---|---|---|---|
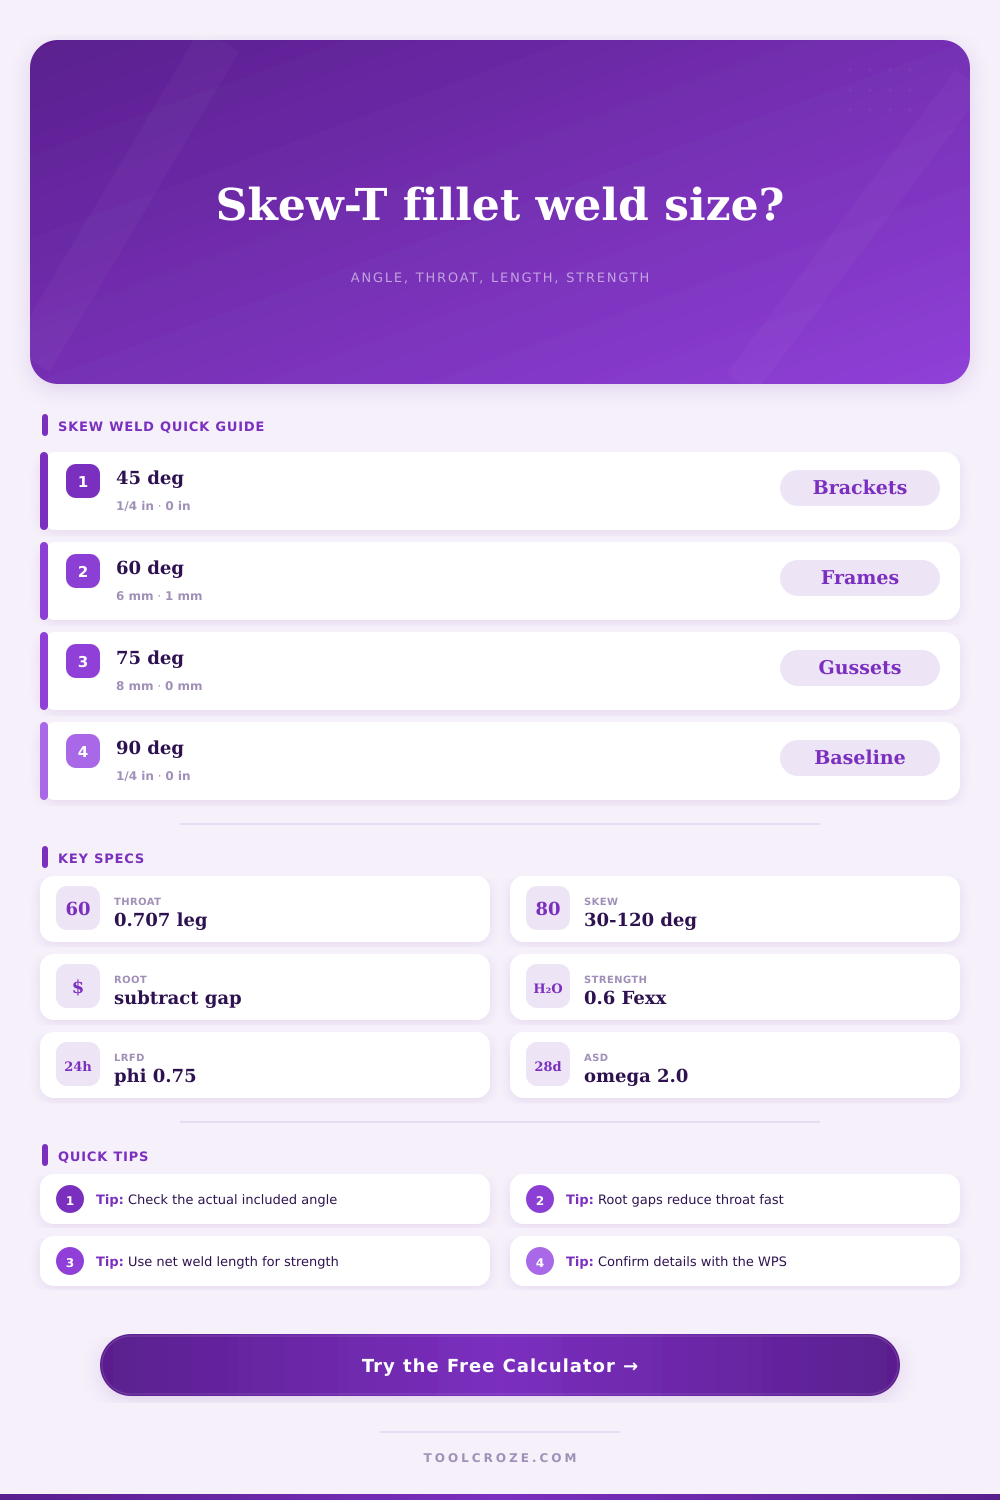
| 30° | 0.966 x leg | Very acute, high theoretical triangle height | Do not take extra credit without detail review |
| 45° | 0.924 x leg | Acute skew, profile and access may control | Root access and contour control are critical |
| 60° | 0.866 x leg | Moderate skew with deeper geometric throat | Confirm whether the code detail allows credit |
| 75° | 0.793 x leg | Mild skew, close to square tee behavior | Good for routine shop and field checks |
| 90° | 0.707 x leg | Standard right-angle fillet geometry | Baseline for common weld schedules |
| 105° | 0.609 x leg | Obtuse joint gives a longer weld face | Throat can drop below the standard shortcut |
| 120° | 0.500 x leg | Wide included angle, shallow triangle height | May require larger legs or a revised detail |
⚡Electrode Strength Reference
| Filler class | Tensile strength | Nominal weld shear | Typical use |
|---|---|---|---|
| E60 | 60 ksi / 414 MPa | 36 ksi / 248 MPa | Legacy or matching lower-strength details |
| E70 | 70 ksi / 483 MPa | 42 ksi / 290 MPa | Common structural steel fillet welds |
| E80 | 80 ksi / 552 MPa | 48 ksi / 331 MPa | Higher strength connection checks |
| E90 | 90 ksi / 621 MPa | 54 ksi / 372 MPa | Special matching-strength applications |
| E100 | 100 ksi / 690 MPa | 60 ksi / 414 MPa | High-strength qualified procedures |
🔧Root Opening and Correction Reference
| Root opening screen | Calculator treatment | Effect on skew throat | Recommended action |
|---|---|---|---|
| 0 to 5% of small leg | Minor deduction only | Usually stable throat estimate | Use measured leg sizes and normal correction |
| 5 to 15% of small leg | Deducts half the gap | Can reduce capacity noticeably | Confirm fit-up and root fusion requirements |
| 15 to 25% of small leg | Deduction plus warning | Net throat may control the whole detail | Consider larger leg or revised joint prep |
| Over 25% of small leg | Severe status flag | Strength estimate may be unreliable | Review with WPS, inspector, or engineer |
🗂Preset Scenario Reference
| Preset | Skew and legs | Load direction | Main check |
|---|---|---|---|
| 90° 1/4 in Baseline | Right-angle equal-leg weld | 30° mixed shear | Compare skew result to standard fillet geometry |
| 45° Angle Bracket | Acute unequal-leg weld | 20° mostly longitudinal | Check throat loss from acute geometry |
| 60° Tube Frame | Moderate skew with root gap | 45° combined loading | Balance field correction and weld length |
| 75° Gusset Tee | Mild skew, larger branch leg | 60° transverse component | Check useful direction factor and utilization |
| Two-Side Column Tab | Double fillet on a tab | 35° mixed shear | Capacity gain from two weld lines |
💡Skew Weld Tips
In theory, most of welds on a structure look easy to calculate from drawings. Just show two plates at a right angle, then say make it a quarter inch fillet and call it good. But things don’t always go so neat in the real world.
Gusset plates, angle brackets, and tube frame fitting isn’t often perfect right angles when you get there. Sometimes the angle between them are different, sometimes one leg is longer than another, and textbook problems with nice neat geometry fall apart. The calculator above do all the trigonometry that will usually slow down site engineer or shop foreman.
Why Real Welds Are Harder to Calculate
Skew joints are great and all, but the core issue is that the standard throat shortcut no longer apply to them. A standard ninety degree fillet effectively has about seventy percent of the throat as its legs. This is a handy number to remember for fillets, but there is one exception: at ninety degrees, the sine equals 1, which isn’t true for any other angle.
As the angle gets tighter (say forty-five degrees) or wider (like one hundred and five degrees), the resulting triangle will change and the resistance to shearing will be less when the width of the triangle increase. Similarly the resistance can seem to grow when the angle closes down, but often you cannot place enough metal in there to make it work. This calculator on the page take your selected skew angle and computes what the real throat is as opposed to having to guess.
Another big one is fit-up: when the two pieces of metal are perfect with no gaps, they touch each other right at the root. This almost never happen in reality. Even a tiny gap between them will reduce the effective throat of weld. If one leg is ten millimeters long and the gap is two, then you’ve got a lot less of what you thought was there before you even fire up. You can enter an allowance for root opening into the calculator, which will reduce calculated throat by a safe measure of that gap.
Why does this matter? Because most people don’t consider this gap and wind up with connections that look great on paper but blow apart under load.
Geometry is also important. Welds that have their long axis loaded parallel to the fillet tend to fail in a different manner different than those loaded perpendicular to their length. Those loaded longitudinally tend to be more ductile (fail by stretching) whereas transversely loaded ones tends to be more brittle (fail by cracking). The calculator allows you to specify the load angle and updates the strength estimate based off this. This allows you to determine whether or not a particular detail can handle the forces it’s going to see. It’s not simply “is the weld large enough?”, rather, “Is it large enough given how I’m going to apply the force?”
It’s also impacted by the fabrication quality and electrode strength. The tool enables you to choose an electrode with a filler metal strength between E60 and E100. Greater electrode strength result in greater nominal shear stress, but doesn’t remedy poor geometry. For instance, if you have a large skew angle resulting in a too-small throat, a higher-strength filler won’t salvage that joint.
And the fabrication correction factor compensate for conditions in the real world. Joints made in the shop are more precise and clean than those fitted in field. A lower fabrication correction factor for a rough fit-up or less-than-ideal access ensures your estimate stays on target.
A couple of reference tables accompany them on a page that puts those input values in context. One table illustrates the throat factor’s relationship with the angle, while another illustrates the effect of gap size on the overall result. It comes into play when you are checking field work or shop drawings and just need to double check something quick. At a glance, you know what size legs would be needed for a forty five degree angle compared to a ninety degree joint, for example, to gain equal strength.
You are working with the unknown. Uncertainty is part of welding. There are so many variables. If it’s wrong it could be real bad. Quantify it. Remove the guesswork. Quantify the load direction, the gap, and the geometry. Now you can think instead of guessing when sizing legs and welding length.
Throat equals strength. Knowing the real throat means the difference between a good joint and one that breaks. Be honest with the geometry. The structure will do the same.