Chip Load Calculator MDF
Calculate MDF CNC chip load, recommended feed, surface speed, material removal rate, heat and dust score, and edge-quality risk from density, bit diameter, flutes, RPM, feed, depth of cut, stepover, and cutter style.
📌MDF Routing Presets
⚙MDF Chip Load Inputs
MDF CNC Chip Load Results
🧱Current MDF and Bit Grid
📊MDF Chip Load Reference
| MDF grade | Density guide | Chip load range | Routing note |
|---|---|---|---|
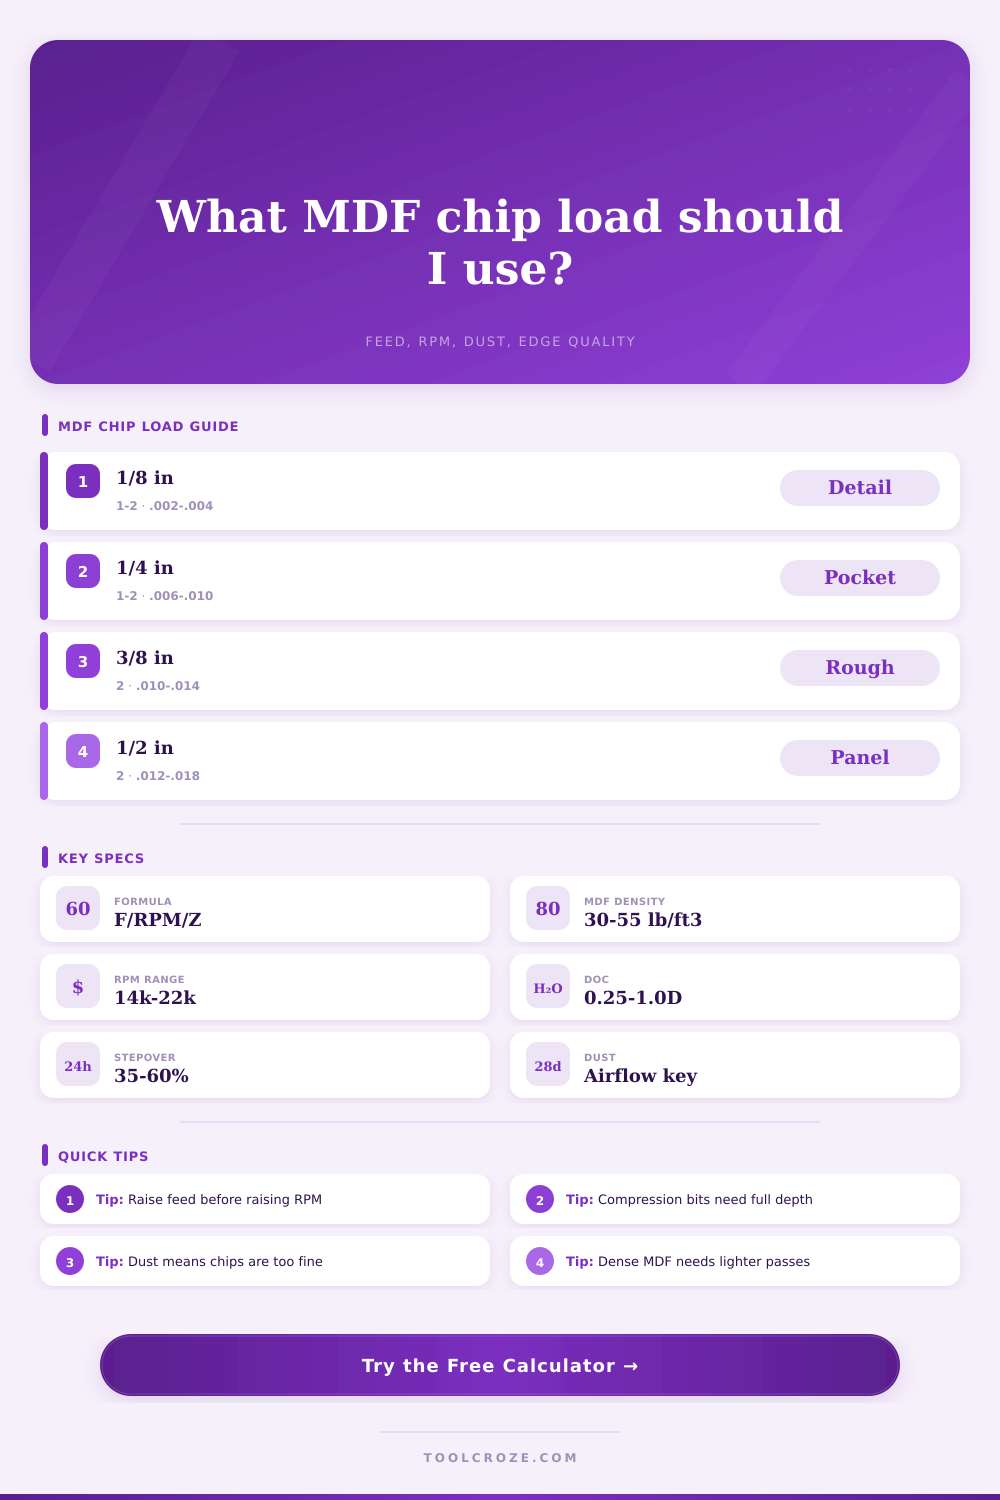
| Ultralight MDF | 30 to 36 lb/ft³ | 0.007 to 0.013 in/tooth | Clears easily but fuzzy edges may need a finish pass. |
| Standard MDF | 38 to 44 lb/ft³ | 0.006 to 0.011 in/tooth | Best all-around setting range for cabinet and sign routing. |
| Dense cabinet MDF | 45 to 50 lb/ft³ | 0.005 to 0.010 in/tooth | Use moderate depth and watch edge heat on long profiles. |
| Moisture-resistant MDF | 42 to 50 lb/ft³ | 0.005 to 0.009 in/tooth | Resins raise heat; a sharp bit and strong dust pull matter. |
| HDF / hardboard core | 50 to 60 lb/ft³ | 0.003 to 0.007 in/tooth | Keep passes lighter and avoid rubbing at high RPM. |
| Laminate-faced MDF | 40 to 52 lb/ft³ | 0.004 to 0.008 in/tooth | Compression or downcut geometry protects the face layers. |
🔪Bit Style and Edge Quality Table
| Bit style | Best MDF use | Chip evacuation | Edge quality note |
|---|---|---|---|
| Upcut spiral | Pockets, dados, roughing | High | Cool cutting and clean lower edge, but the top can fuzz. |
| Downcut spiral | Top-face quality | Low to medium | Excellent top edge, higher heat risk in deep closed slots. |
| Compression spiral | Through-cut sheet goods | Medium | Clean top and bottom when depth passes engage both spirals. |
| Straight flute | Simple profiles | Medium | Stable but less efficient at dust evacuation than spirals. |
| Surfacing cutter | Flattening faces | High airflow needed | Use shallow DOC and wide stepover for low ridge marks. |
| Engraving bit | Letters, inlays, shallow marks | Low | Small chips become dust fast; feed enough to avoid rubbing. |
⚙Diameter, Flute, and Feed Grid
| Bit diameter | Flutes | 18,000 RPM feed | Typical MDF operation |
|---|---|---|---|
| 1/8 in / 3.175 mm | 1 flute | 36 to 72 in/min | Small pockets, letters, template details. |
| 1/8 in / 3.175 mm | 2 flutes | 72 to 120 in/min | Detail profiles when dust collection is strong. |
| 1/4 in / 6.35 mm | 1 flute | 110 to 180 in/min | Cleaner chip size on hobby routers. |
| 1/4 in / 6.35 mm | 2 flutes | 200 to 360 in/min | Cabinet pockets, through-cuts, nested sheets. |
| 3/8 in / 9.525 mm | 2 flutes | 320 to 500 in/min | Roughing and wider dados on rigid machines. |
| 1/2 in / 12.7 mm | 2 flutes | 430 to 650 in/min | Panel sizing, surfacing, and production routing. |
📋MDF Preset Settings Table
| Preset | Bit and RPM | Feed and DOC | Quality target |
|---|---|---|---|
| 1/4 upcut pocket | 0.25 in, 2 flute, 18k | 220 in/min, 0.25 in DOC | Fast chip clearing with manageable dust. |
| Compression panel | 0.25 in, 2 flute, 18k | 260 in/min, 0.35 in DOC | Clean top and bottom on sheet edges. |
| Downcut laminate skin | 0.25 in, 2 flute, 20k | 170 in/min, 0.08 in DOC | Top-face chip control on coated MDF. |
| HDF shallow engrave | 0.125 in, 1 flute, 20k | 55 in/min, 0.03 in DOC | Lower edge heat while keeping fine detail. |
💡MDF Routing Tips
Ever watch a CNC machine cut out a smooth piece of MDF only for that cut to go coarse? You didn’t change anything on your setup. Nothing changed… Except the cut. Suddenly there’s fine dust everywhere, Edges is chipping away. Maybe you even notice your bit is smoking. But nothing is wrong with the code, no part of the machine are broken. The variable is the chip load, which drift off target. That variable will make the difference between a perfect cut and a ruined panel.
Knowing what to set depends more than guessing at a spindle speed. The calculator above figures it out for you. Translating raw diameter and density to feed rates is one thing, using them are another. And that’s the main point. What do these numbers mean?
What is Chip Load and Why It Matters
The first is chip load. Simply put, how much material does each flute remove on each revolution? Too little and the bit starts rubbing rather than cutting. Friction creates heat. MDF is essentially a glue-impregnated pile of sawdust. MDF hates heat. Heat causes the glue to soften and edges start to fuzz. Your dust collector fills up with powdered dust, not chips. You raise your feed rate and you get a cooler, cleaner cut. A slower feed rate make the bit hotter. Counterintuitive, right? It works.
That’s where your bit diameter comes into play and completely changes the geometry. At equal RPM, the outer edge of a half inch cutter will go farther around in one rotation than a quarter inch bit. The reference table on the page lay it all out. It explains that larger diameters will remove more material volume but must be fed at higher rates to maintain same chip thickness. If you drop your feed rate while keeping the RPM high, you’re asking each tooth to take a tiny bite. Tooth don’t cut, tooth grinds. You get a burn mark which cannot be removed by sanding.
Surprisingly, this has a lot to do with dust collection. While cutting, lots of guys only pay attention to their cuts and doesn’t think about air flow at all. Dust from MDF is dense and fine. That stuff will hang around until someone sucks it up. Poor dust collection means you have to go slower to prevent overheating. That reduces your effective chip load. It is a vicious cycle. Go slow because dust collects, More friction lead to higher temperatures. Higher temperature makes the bit hotter. Extract well and it carry the heat off along with the chips and breaks the cycle.
Size is important, but so is bit style. The upcut spiral cuts well in deep pockets and cleans out chips nicely, but will tear surface veneer on laminated medium-density fiberboard. A downcut bit pushes the material down and thus protects leading edge, but tends to hold chips in the cut. That leads to increased heat build-up. Then there are compression bits that attempt to do both. There’s upcut at the bottom and downcut at the top. For through-cuts, they are beautiful. If you go deep enough into the cut to engage both sets of flutes. Otherwise, shallow cuts with a compression bit don’t live up to their potential and are often no better than a straight upcut spiral.
The last levers we pull on are depth of cut and stepover. To take a deep plunge, you need a lighter chip load per tooth to avoid buckling the bit. To run wide stepovers, you need move the tool faster to maintain sharpness of the cutting edges. It’s all about balance. You’re always trading off density for durability and speed for surface finish.
The calculator could of helped you get there, but your eyes and ears will confirm. What does it sound like? Listen for the pitch of the cut. If it’s a high pitched scream, you know it’s rubbing. If it’s a steady roar, then you know it’s biting. Listen for the sound and trust it. When the dust becomes chunky chips and the pitch lowers again, you’ve hit the sweet spot. The machine is doing exactly as it was asked. It’s taking away material efficienty while not fighting itself. That’s what a perfect chip load sounds like.