CNC Plasma Cutting Speed Calculator
Estimate cut speed, travel time, pierce delay, lead-in length, kerf compensation, arc voltage range, and duty cycle load for common CNC plasma cutting setups.
📌Plasma Cutting Presets
⚙CNC Plasma Inputs
CNC Plasma Cutting Results
📊Selected Process Window
🔬Plasma Material Grid
| Material | Speed Factor | Kerf Behavior | Cut Quality Note |
|---|---|---|---|
| Mild steel | 100 percent baseline | Predictable narrow to medium kerf | Use as the base chart for plate and sheet settings |
| Stainless steel | About 70 percent of mild steel | Slightly wider dross-prone kerf | Often needs slower travel and close torch-height control |
| Aluminum | About 80 percent of mild steel | Wider shiny kerf, fast heat spread | Keep travel steady to reduce top bevel and recast |
| Copper / brass | About 55 to 70 percent of mild steel | Variable kerf due to high conductivity | Use conservative speed and verify edge quality on scrap |
| Titanium | About 45 percent of mild steel | Narrow but heat-sensitive kerf | Use low heat input and avoid lingering at starts |
| AR plate | About 85 percent of mild steel | Medium kerf with harder slag | Slower speed can improve bottom edge release |
⚡Amperage and Thickness Reference
| Mild Steel Thickness | Common Amps | Cut Speed Range | Typical Kerf |
|---|---|---|---|
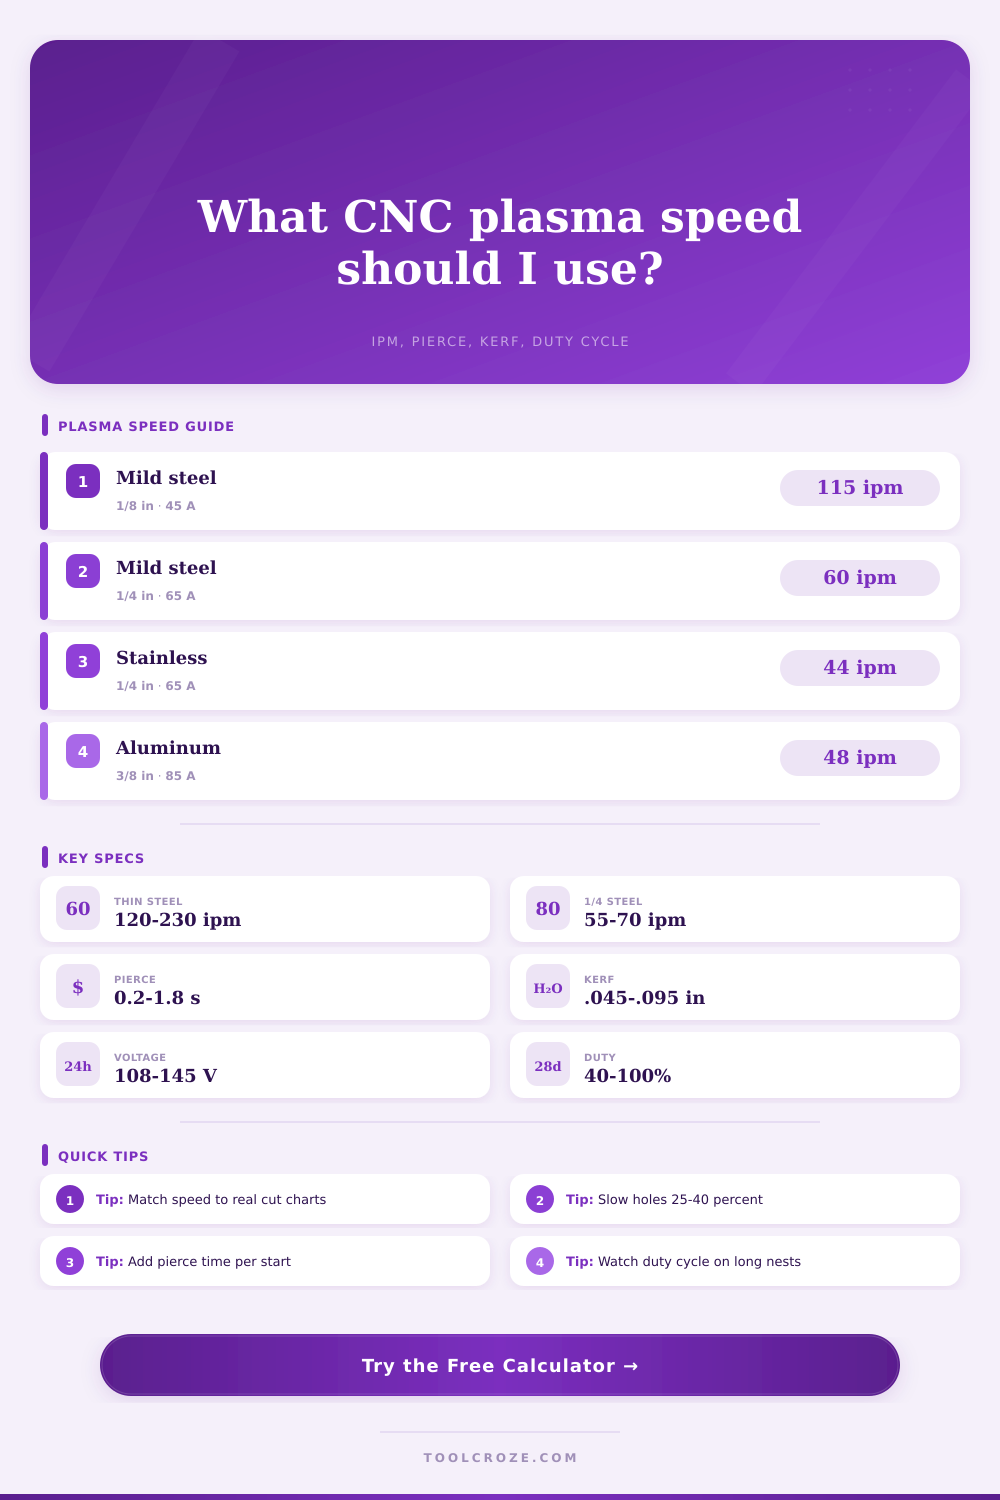
| 16 ga / 0.060 in / 1.5 mm | 30 A | 180 to 230 IPM / 4570 to 5840 mm/min | 0.045 to 0.050 in |
| 1/8 in / 3.2 mm | 45 A | 100 to 140 IPM / 2540 to 3560 mm/min | 0.055 to 0.065 in |
| 1/4 in / 6.4 mm | 65 A | 55 to 70 IPM / 1400 to 1780 mm/min | 0.065 to 0.075 in |
| 3/8 in / 9.5 mm | 85 A | 40 to 55 IPM / 1020 to 1400 mm/min | 0.075 to 0.085 in |
| 1/2 in / 12.7 mm | 85 to 105 A | 26 to 38 IPM / 660 to 965 mm/min | 0.085 to 0.100 in |
| 3/4 in / 19 mm | 125 A or higher | 14 to 24 IPM / 355 to 610 mm/min | 0.100 to 0.125 in |
🔧Cut Style Adjustment Table
| Cut Style | Speed Multiplier | Lead-In Planning | Best Result Target |
|---|---|---|---|
| Outside or inside profile | 100 percent | Normal straight or arc lead-in | Balanced edge angle and bottom dross |
| Long straight cut | 105 percent | Lead in from scrap side when possible | Lower heat input on simple straight paths |
| Small holes and slots | 65 percent | Shorter lead-in with centerline compensation | Round holes with less taper |
| Fine detail / thin web | 78 percent | Use lead-ins that avoid fragile webs | Reduced corner washout and better detail |
| Bevel or angled cut | 72 percent | Longer lead-in helps stabilize arc angle | Cleaner bevel face and steadier torch height |
| Expanded metal / grate | 55 percent | Expect frequent restarts and interrupted arcs | Reliable restart behavior more than edge finish |
📝Voltage, Pierce, and Duty Reference
| Process Window | Arc Voltage | Pierce Delay | Duty Cycle Watch |
|---|---|---|---|
| 30 A thin sheet | 105 to 118 V | 0.10 to 0.25 sec | Short nests rarely stress a 60 percent machine |
| 45 A general sheet | 118 to 128 V | 0.25 to 0.55 sec | Many pierces add heat even when travel is short |
| 65 A plate | 125 to 138 V | 0.60 to 1.00 sec | Long profiles can exceed a 50 percent duty limit |
| 85 A heavy plate | 132 to 148 V | 0.90 to 1.70 sec | Plan cooling rests between large nested sheets |
| 105 A plus | 140 to 165 V | 1.30 to 2.50 sec | Use the rated duty chart for the exact current |
💡Plasma Speed Tips
When you have a plasma cutter humming along it has a distinctive tone. Kind of like a jet plane idling on the tarmac. A nice, steady high pitched hiss. Too slow? The sound warbles. Too fast? The arc sputters and there’s a jagged lip left on bottom of the material. The right speed take some combination of science and trial and error.
Once you enter the amperage and material thickness into our tool above, the rest of calculations happen automatically using a basic math equation. You won’t have to guess with conversions and coefficients anymore.
How the Calculator Works
Most operators only care about cutting speed, which is measured in inches per minute. They use speed as a throttle, turning it up until they cannot cut. This is a mistake. Speed is just one factor in a thermal equation involving travel distance, pierce time, and machine duty cycle.
The tool take all these into consideration. It figures out how long your entire path are going to be and then tallies up the seconds required to pierce every hole along the way. Delays from piercing often rob you of efficiency. You might have hundreds of little bracket nested and the actual cutting time might be short. But the machine sits there waiting half the cycle for the arcs to take hold. The calculator totals up this delay too so you can see the true time price of doing business.
There’s also the fact that amperage dictate speed, and amperage is dictated by material thickness. You can’t cut a sixth inch of mild steel just as fast as you can cut a sixth-inch-thick piece of it, no matter how many amps you throw into the machine. The energy density have limits, and thicker materials require more current to penetrate. The thinner the material, the wider range of speeds it will accept. Too much speed on thick stuff means that arc doesn’t get enough time to heat through the full depth. The amount of current going through determines penetration. And the greater the thickness, the smaller the window of allowable speeds become.
The chart on the page lists speed based off thickness. Notice that as thickness goes up, speed go down. This is not because amps go down (the opposite), but because the range of safe speeds shrinks. This isn’t a straight line, either. It’s a cliff. A small increase in thickness can slash your allowable speed by half.
Another thing that gets novices: kerf width. You cut, then there’s a hole. How did it get there? Because the plasma stream take out material. Kerf is name of the slot where material went. For tight tolerance parts, remember to include that kerf in your design. The estimate includes the kerf area as defined by typical consumables width. So you can see roughly what amount of metal will become slag and smoke. That’s good for estimating stock needs and making sure fitted part match. Ignoring kerf is how you end up with a frame that doesn’t fit.
It’s also got something called Duty Cycle. Essentially, this means how long a machine will go before it gets so hot it shuts itself off. When you’re cutting steel, it heat up like crazy. A 60 percent duty cycle machine means you’ve got six minutes out of ten where you can be cutting. For the other four minutes, the torch has to be cool. You choose the duration of your duty cycle window, and the tool monitors how long your torch is on (arc-on time) to tell you if you’re trying to do too much with your hardware. That knowledge could of prevented you from shutting down in the middle of a job, which wastes a whole stack of pricey stainless steel.
Not all metals are created equal. Mild steel isn’t like stainless steel or aluminum. Those two materials transfer heat more quickly and sometimes also needs to be run at a slower speed for good cuts. Based off your selected material in the calculator, the base speed will adjust.
For example, with aluminum, you’ll see that the cut edge looks good because it’s shiny and reflective. However, it can hide dross. When you think it cut well its really not so good under there. By slowing down just a bit, you’re able to get better quality on the bottom edge of those alloys. It’s a subtle change but it’s what makes the difference between a clean part and needing it ground out.
You get better at shop time with experience. If it’s a rusty or rough plate, maybe reduce your speed override percentage to ninety percent. Arcs behave different than different surfaces. Theoretical ideal comes from the calculator. Reality comes through your eyes and ears. Get near the right number with the tool then let the arc tune itself out as you listen for that solid hiss. That’s what you’re after.
All the rest is just noise.