Inverse Time Feed Rate Calculator
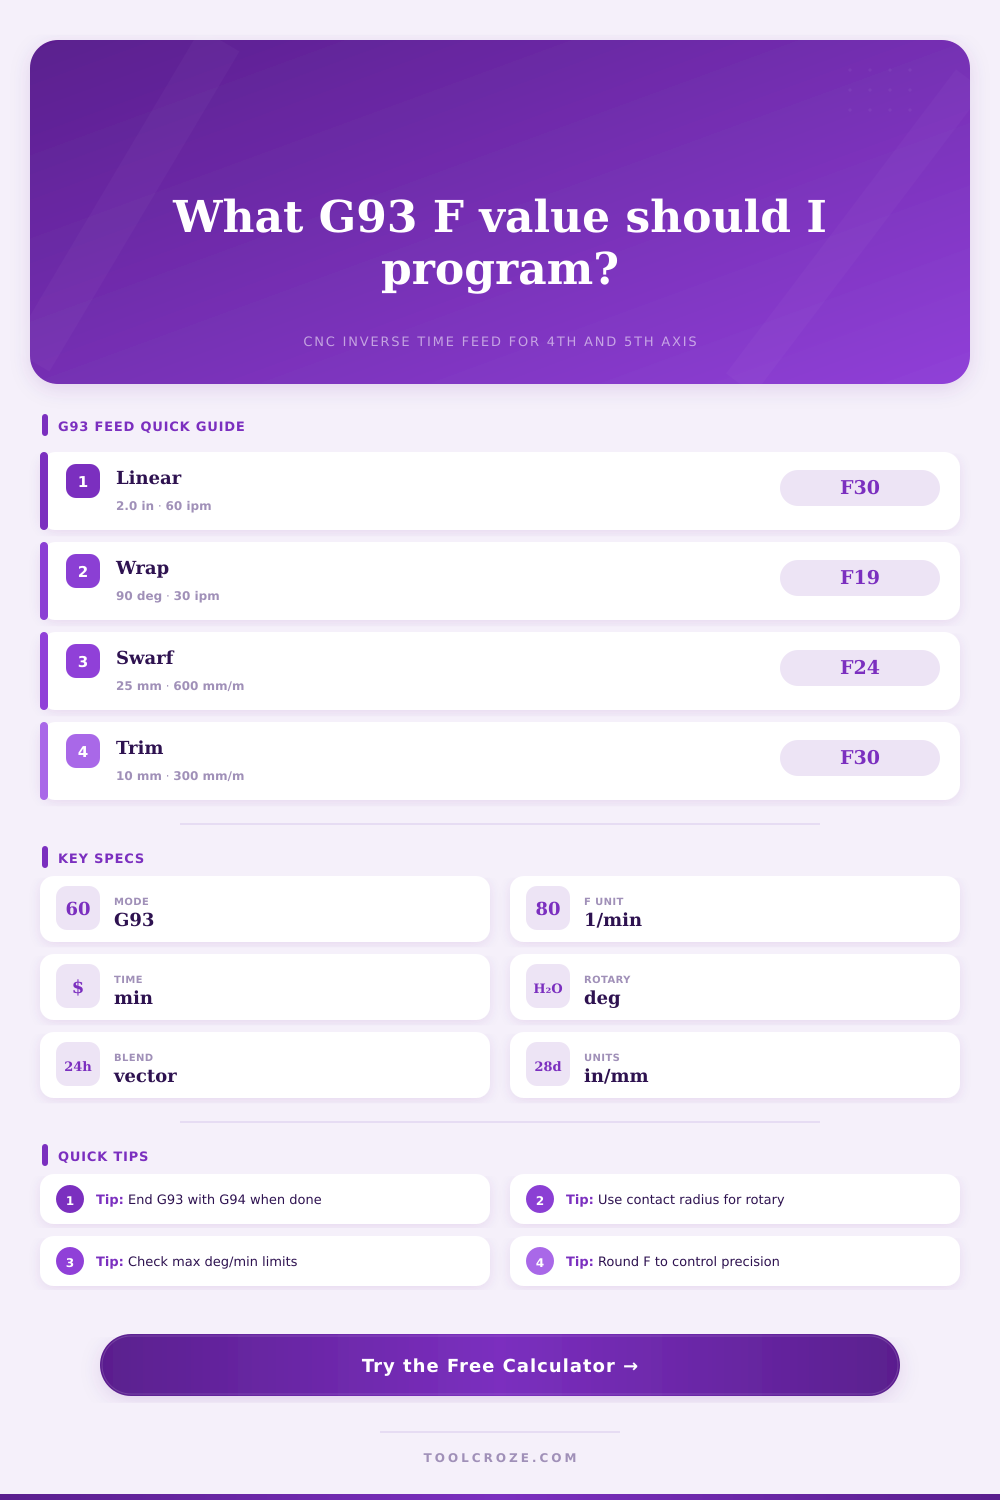
Calculate CNC G93 inverse time F values from linear distance, rotary degrees, contact radius, desired feed, blended axis length, machine units, cycle time, and rotary surface speed.
📌4th and 5th Axis Presets
⚙G93 Feed Inputs
Inverse Time Feed Results
📊Machine and Program Spec Grid
📐G93 Formula Reference
| Calculation | Formula | Use When | Result Unit |
|---|---|---|---|
| Linear length | sqrt(X² + Y² + Z²) | XYZ endpoint deltas are known | in or mm |
| Rotary arc | radius x degrees x pi / 180 | A, B, or C changes contact radius | in or mm |
| Blended length | sqrt(linear² + rotary arc²) | Linear and rotary axes cut together | in or mm |
| G93 inverse feed | F = feed / effective length | Programmed F is inverse minutes | 1/min |
| Block time | minutes = 1 / F | Estimate single move time | min or sec |
⚒Rotary Radius and Surface Speed Guide
| Setup | Typical Radius | 90° Arc Length | Programming Note |
|---|---|---|---|
| Small 4th-axis part | 12 mm / 0.47 in | 18.8 mm / 0.74 in | Engraving and fine wrap moves |
| Tube or shaft wrap | 25 mm / 0.98 in | 39.3 mm / 1.55 in | Use part OD contact radius |
| Medium trunnion work | 75 mm / 2.95 in | 117.8 mm / 4.64 in | Tool-center point may alter radius |
| Large mold or fixture | 150 mm / 5.91 in | 235.6 mm / 9.27 in | Rotary motion can dominate feed |
🎯Controller and Machine Check Table
| Check | Common Range | Why It Matters | Action |
|---|---|---|---|
| F precision | 0 to 4 decimals | Rounding changes short block time | Match post output format |
| Rotary rate | 1000 to 20000 deg/min | Axis speed may limit finish | Compare with machine spec |
| Shortest block | 0.01 to 0.20 sec | Very tiny blocks can starve lookahead | Smooth or merge segments |
| Mode reset | G94 after G93 | Later feed words return to units/min | Post clear modal changes |
🗂Preset Move Examples
| Preset | Move Style | Feed Target | Typical Output |
|---|---|---|---|
| A Wrap Aluminum | 4th-axis helical blend | 600 mm/min | Moderate F, surface checked |
| Trunnion Trim | B/C simultaneous tilt | 450 mm/min | Rotary arc dominates |
| Cylinder Engrave | Small-radius wrap | 25 ipm | Short fast G93 blocks |
| Blade 5-Axis | XYZ plus A/B motion | 320 mm/min | Low F for smooth finish |
💡Inverse Time Feed Tips
Programming a block of G-code appears easy enough when working with only linear axes but as soon as you work on a trunnion or rotary table it become more complex. It’s no longer inches per minute; instead, it is how fast the cutter actualy moves over the part.
That transition is handled through inverse time feed rate. Rather than commanding an axis at a certain speed, you are commanding it for a period of time. If you put in the rotary angle and length of each segment, the calculator do the math. It eliminates the guesswork on what conversion factors and coefficients does, which tends to confuse new programmer.
Why Inverse Time Feed Rate is Important
That’s the basic idea: an inversion of intuition. Typically you command your controller to go sixty inches a minute in whatever direction you’re moving. That means the controller know the distance divided by time (speed). Inverse time feed flips it around, you specify the length of time for the move. The controller computes what velocity each axis need to reach to complete the motion in requested time.
That’s important if there is multiple axes being moved simultaneously. For example, a five-axis move could be a big rotary sweep with a tiny linear step. Commanding a constant linear feed rate might require the rotary axis spinning far too quickly to maintain pace. With inverse time programming, the machine spread out the load. It keeps all axes within their mechanical limits yet provides a steady surface speed.
The biggest mistakes is made by neglecting contact radius. The farther away the cutter is from the center of rotation, the more distance it cover when rotated on the fourth axis. A 10 degree turn is a short hop up close to the nose of the spindle. At the end of a long fixture it’s a long arc. Depending based off the radius you enter for calculation, the calculator turns the angular movement into the matching linear arc length.
Without this translation there is no way you can set the correct feed rate. You’ll have too high or low a rate and suffer bad finish or worn tools. A little thing but it makes all the difference in the cut.
You can combine both rotary distance and linear distance with the tool. That’s important when creating a complex contour that has the tool traveling in a diagonal direction in space. Think of it as the hypotenuse of your rotary arc plus your linear travel. Feed it at one or the other rate and you risk overfeeding along combined path. The formulas are clear from the page’s reference table. They show how linear length, rotary arc, and blended length affect the resulting F value.
Another important factor to consider is the precision of controllers. Older machines might only take integers as an F word parameter. Today’s high speed controls can have multiple decimal places. On small moves, rounding errors multiply rapidy. Having an Inverse feed that’s off by 0.001 makes all the difference in the world on a small portion of the part; it may be a smooth or a chatter mark.
Match your programmed precision to the support of your post-processor. With the calculator, you can toggle this setting so your results reflect reality.
Another advantage is estimating cycle time. How long will this part take? How much time per segment? That’s good for both scheduling as well as for quoting jobs. And it also shows where bottlenecks may be emerging. For example, if one of your blocks proves way slower then the rest, perhaps that’s because the toolpath is inefficient, or maybe you have an unnecessarily slow feed rate. Adjust the inputs and see what happens when you change the desired surface speed.
Once finished, make sure you return to normal feed mode. If the programmer fails to return the controller back to G94 and leaves it in G93 mode, some later block will have unexpected results. It’s modal, meaning it stays set unless overridden. To prevent problems, simply include a G94 at the end of whatever program you’re working on.
It separates machine kinematics from programming. Tell the machine where you’d like it to go, let it work out the details of how to get there. Think in terms of time rather then speed. It takes some mental adjustment but the payoff would of been well worth it. Cycle times becomes repeatable, tools last longer, and parts have a smoother finish.
The key is knowing what you’re measuring. Once you start thinking in seconds per move instead of inches per minute, everything just clicks into place.