CNC Feed Rate Calculator for Wood
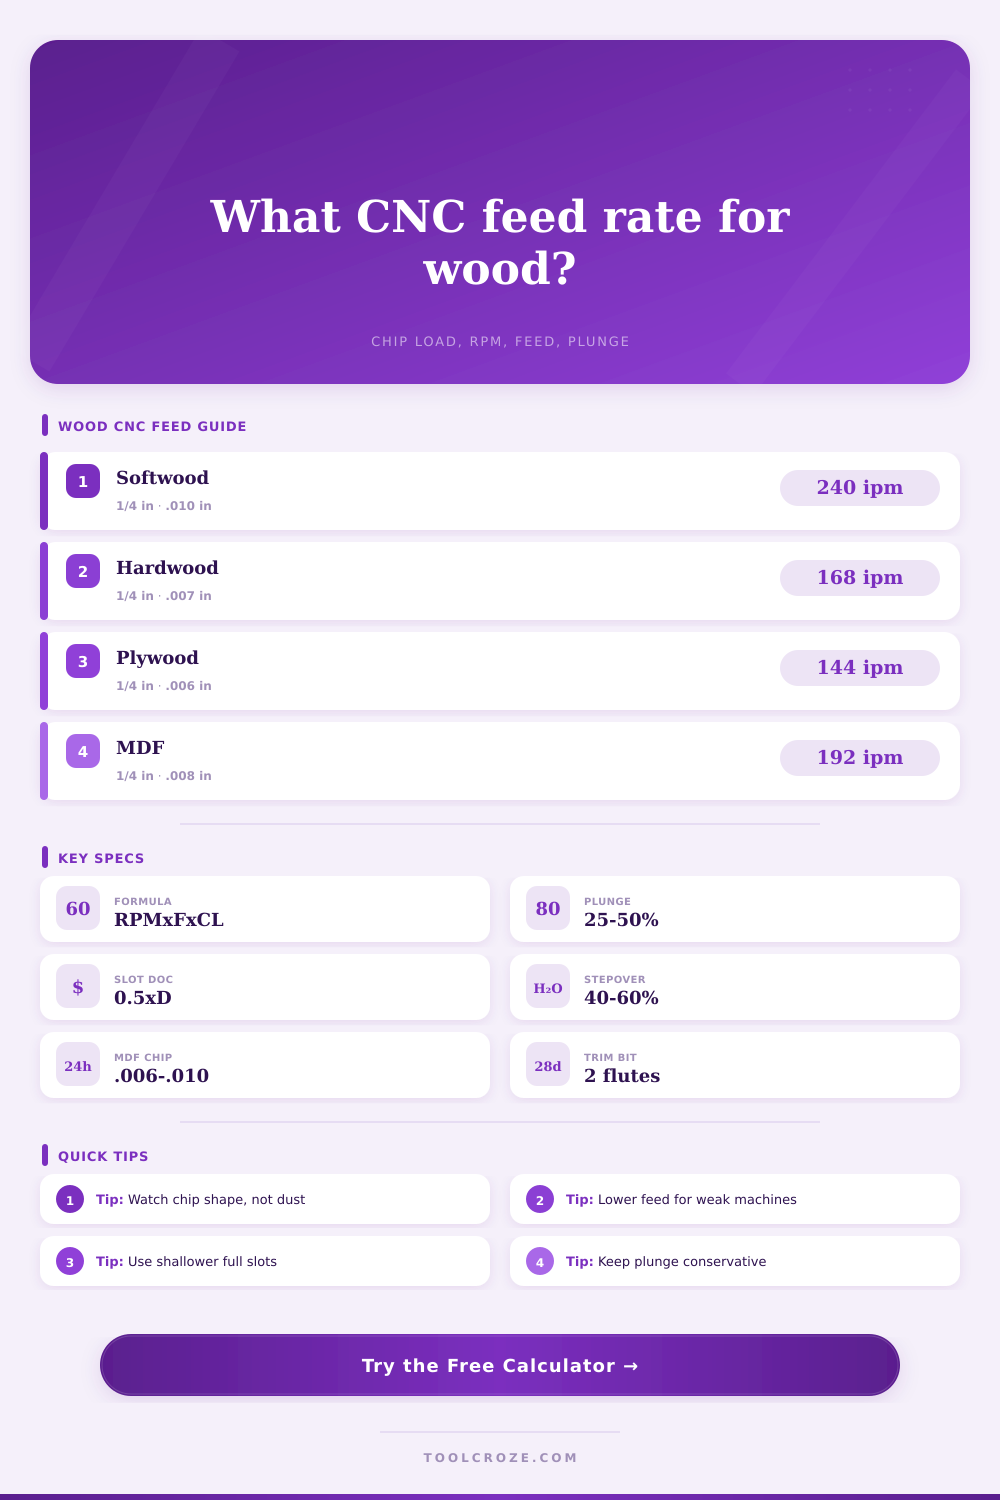
Estimate wood routing feed rate from bit diameter, flute count, RPM, chip load, depth of cut, stepover, machine rigidity, and toolpath length.
🎛Wood CNC presets
⚙Routing inputs
CNC wood routing result
📊Material and bit spec grid
🌳Wood chip-load reference
| Material | 1/8 in bit | 1/4 in bit | 3/8 in bit | Typical RPM |
|---|---|---|---|---|
| Softwood / pine | 0.003-0.005 in | 0.008-0.012 in | 0.010-0.016 in | 16000-22000 |
| Cedar / cypress | 0.003-0.006 in | 0.009-0.014 in | 0.012-0.018 in | 16000-22000 |
| General hardwood | 0.002-0.004 in | 0.005-0.009 in | 0.008-0.012 in | 14000-20000 |
| Hard maple | 0.002-0.003 in | 0.004-0.007 in | 0.006-0.010 in | 13000-18000 |
| Plywood | 0.002-0.004 in | 0.005-0.008 in | 0.007-0.011 in | 16000-21000 |
| MDF / HDF | 0.003-0.005 in | 0.006-0.010 in | 0.009-0.013 in | 16000-22000 |
| Laminated plywood | 0.002-0.003 in | 0.004-0.007 in | 0.006-0.010 in | 15000-20000 |
🔩Bit selection reference
| Bit style | Best use | Flutes | DOC starter | Stepover |
|---|---|---|---|---|
| 1/8 in upcut spiral | Small pockets, roughing | 1-2 | 0.04-0.08 in | 30-45% |
| 1/4 in upcut spiral | Fast clearing, solid wood | 2 | 0.10-0.18 in | 40-60% |
| 1/4 in downcut spiral | Clean top edge | 2 | 0.06-0.12 in | 35-50% |
| 1/4 in compression | Plywood through cuts | 2 | 0.12-0.20 in | 80-100% |
| 3/8 in roughing bit | Large pockets, slabs | 2-3 | 0.18-0.30 in | 45-65% |
| 60 degree V-bit | Engraving, signs | 1-2 | 0.01-0.05 in | 10-30% |
⏱Preset feed examples
| Job | Material | Bit | RPM | Starting feed |
|---|---|---|---|---|
| Cabinet pocket | Pine | 1/4 in 2F | 18000 | 210 ipm |
| Hardwood contour | Oak | 1/4 in 2F | 16000 | 125 ipm |
| Sheet cutout | Plywood | 1/4 in 2F | 18000 | 135 ipm |
| MDF slot | MDF | 1/4 in 2F | 18000 | 145 ipm |
| Detail carving | Cedar | 1/16 in 1F | 20000 | 45 ipm |
| Slab roughing | Walnut | 3/8 in 2F | 14000 | 160 ipm |
📐Operation adjustment table
| Operation | Feed factor | Plunge factor | DOC cue | Chip cue |
|---|---|---|---|---|
| Profile / contour | 1.00 | 35% | 0.5xD to 0.75xD | Medium chip |
| Full-width slot | 0.75 | 25% | 0.35xD to 0.55xD | Clear chips |
| Pocket clearing | 1.05 | 40% | 0.5xD to 1.0xD | Steady chips |
| Adaptive clearing | 1.20 | 45% | 1.0xD to 1.5xD | Low radial load |
| Light finish pass | 0.85 | 30% | 0.1xD to 0.25xD | Light shaving |
| V-carve / engraving | 0.60 | 25% | Shallow pass | No burning |
💡Routing tips
Don’t guess your feed rate… This will both dull your tool and damage your wood. Burning toast smelling wood and a screaming spindle are signs your feed rate is probably wrong. CNC operators get their speeds and feeds based off forums, but they’re not abstract; they’re mechanical. The amount of force applied to the cutting edge has to be managed.
Too slow and the bit won’t cut; it’ll just rub against the material. Friction create heat which dulls your bit and damages your wood. Too fast and the bit breaks and the machine vibrate.
Why You Should Use a Calculator for CNC Speeds and Feeds
Once you enter the RPM and bit diameter, calculator does the rest for you. No more guessing about conversions or coefficients. The tool takes your physical constraints and gives you a safe operating window. Now you can focus on what you want to do with your cut.
The main factor here is chip load, which is thickness of wood chip removed by each flute with every turn of the cutterhead. You need the chip to be thick enough to transport heat away from the cutting edge. If it’s fine like dust, then you’re running too slow for the speed. The feed isn’t matching the speed and you’re sanding the wood instead of slicing it. That’s a pretty common error, as people think that more RPM is always good. Running at a higher RPM but not feeding at an equal or greater rate creates nothing but friction.
The chart of reference will give you examples of how much chip load different materials need. Hard maple needs a thinner chip than soft pine because its fibers are denser. Because the fibers aren’t as dense as hard maple, theyll accept a thicker chip before overheating. You must adjust your target chip load for each material.
How far does the bit engage into the wood, one turn at a time? That’s depth of cut times stepover. The more it engages (a deeper axial cut), the more stress are applied to the length of the bit. The wider the radial stepover, the more leverage there is on the shaft. To get maximum feed with either one, you have to compromise the other; otherwise the bit will chatter or break.
The tool takes that into account by figuring out how fast it can removes material given your chosen engagement level. If it’s a finish pass, it’ll use slower rates than if it’s a roughing pass. Buttons on the tool let you preset things so they adapt automatically for each operation, such as clearing pockets. In each case, the tool act differently. With adaptive clearing, the radial engagement stay low while allowing deeper cuts and faster feeds.
Rigidity is a tough one to figure out. An industrial router mounted on a beefy frame can take some aggressive feeds without skipping a beat, while the same model on a lightweight desk might be shaken senseless. For this reason, there’s a rigidity factor in the calculator. If your machine has a light frame it’ll scale back recommended feed rates accordingly. That makes sense because the machine structure forms part of the cutting system. All the right RPMs and bits won’t help if your gantry flexes like jello. Often you need to back off the feed rate to stay within the limits of your machine structure, and that’s where the line between a good cut and part-goner is drawn.
Feed and plunge rates are sometimes forgotten unless something go wrong. Why plunge differently? The plunge feed is special because it’s cut by the center point of the bit. The center point do not move forward. Typically, the plunge feed rate is a fraction of the lateral feed rate. A lower plunge feed prevents the bit from grabbing or burning the entry point. That’s important when starting in pockets.
It also gives you time estimates so that you know how long a pocket should take and can then be able to plan out job work. If I know a pocket will be ten minutes, I can better manage my use of resources such as coolant or dust collection. But that’s just a number. I think it’s best to let the machine talk to you to get the right setting. If it’s humming smoothly and consistently, then you’re probably on the right speed. If it sounds like a high pitched squeal, it is too slow. If it sounds like a loud thumping noise, you’re cutting too deep or your feed is too fast.
Take the numbers as a guide. And go from there adjusting according to what you are seeing and hearing. You want minimal heat and a clean cut. That means the bit stays sharp and the wood comes off smooth. It also makes for a quieter machine.
Math tells you where to start. Your ears tell you when to stop.