Cylindrical Grinding Speeds and Feeds Calculator
Estimate wheel surface speed, workpiece RPM, traverse feed, radial infeed, stock removal, spark-out allowance, and cycle time for OD cylindrical grinding.
⚙ Cylindrical Grinding Presets
📏 Setup Inputs
Grinding Results
🧱 Wheel and Material Grid
📊 Speed Reference Tables
| Material | Common Wheel | Wheel Surface Speed | Work Surface Speed |
|---|---|---|---|
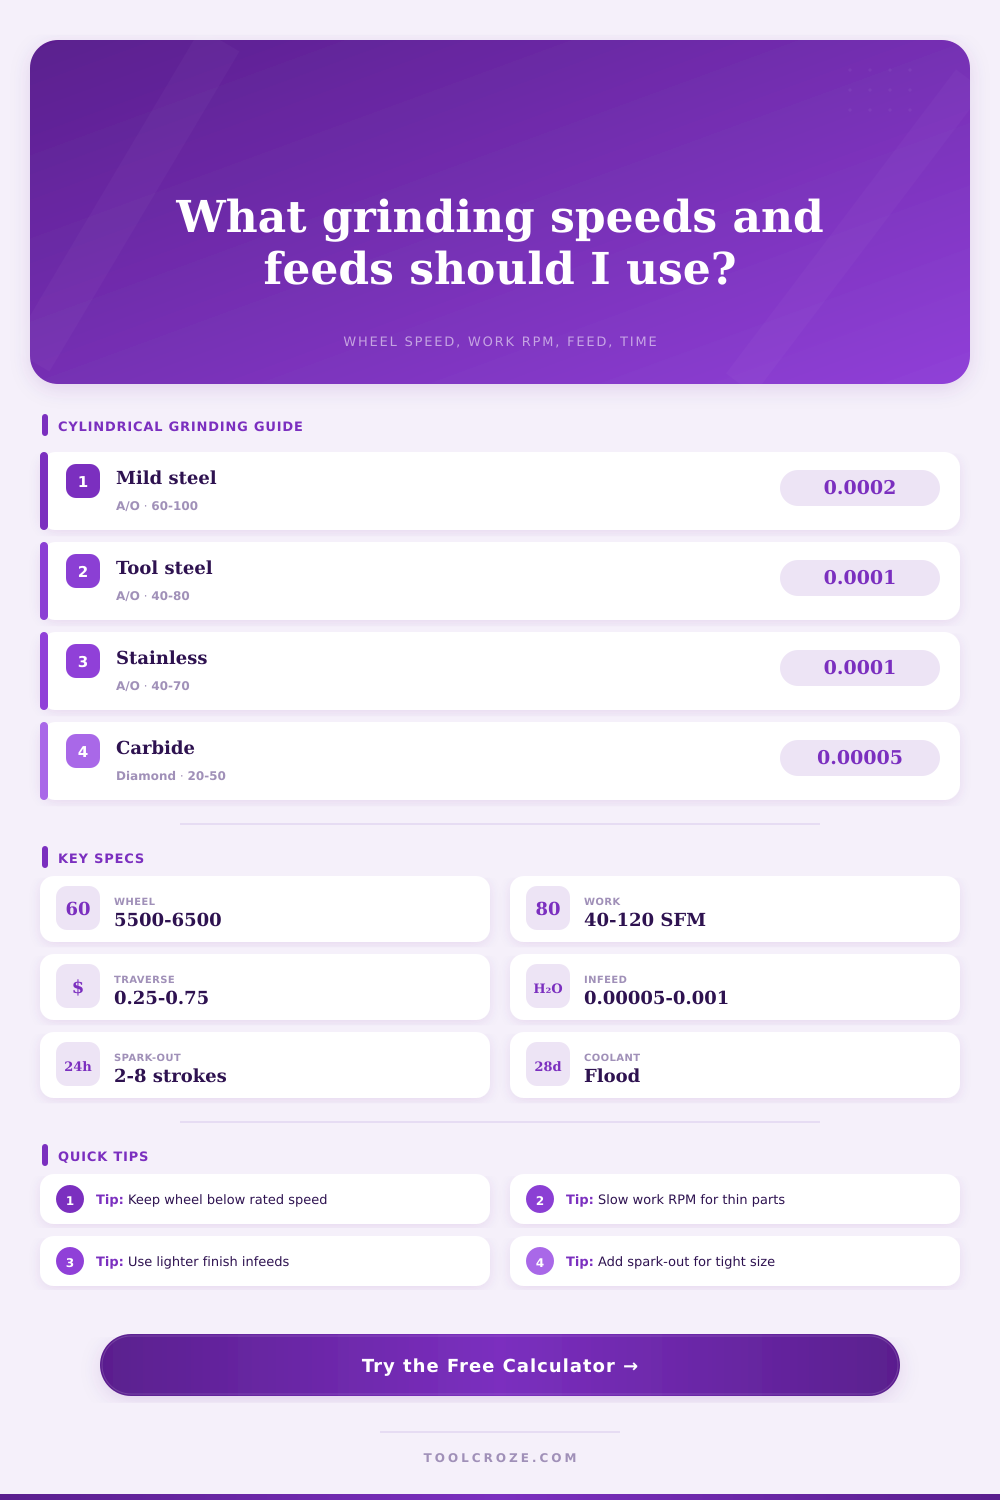
| Mild steel | Aluminum oxide 46-80 grit | 5,500-6,500 SFM | 60-100 SFM |
| Hardened steel | Aluminum oxide, ceramic, or CBN | 5,000-6,500 SFM | 40-80 SFM |
| Stainless steel | Friable aluminum oxide | 4,800-6,000 SFM | 40-70 SFM |
| Cast iron | Silicon carbide or aluminum oxide | 5,000-6,500 SFM | 70-120 SFM |
| Carbide | Diamond resin or vitrified diamond | 4,000-6,000 SFM | 20-50 SFM |
| Operation | Infeed Per Pass | Traverse Per Work Rev | Spark-Out |
|---|---|---|---|
| Rough OD traverse | 0.0003-0.0010 in radial | 0.50-0.75 wheel width | 1-3 strokes |
| Finish OD traverse | 0.0001-0.0004 in radial | 0.25-0.50 wheel width | 3-6 strokes |
| Thin part or small pin | 0.00005-0.0002 in radial | 0.20-0.40 wheel width | 4-8 strokes |
| Hard chrome finish | 0.00005-0.0002 in radial | 0.25-0.45 wheel width | 5-10 strokes |
🔧 Wheel / Material Selection
| Work Material | Abrasive Choice | Typical Grade | Coolant Note |
|---|---|---|---|
| Low carbon and mild steel | Aluminum oxide | 46-80 grit, medium grade | Flood coolant for finish stability |
| Hardened bearing steel | CBN or seeded gel | 80-120 grit, open structure | Keep heat out of the surface |
| Stainless steel | Friable aluminum oxide | 60-100 grit, softer grade | Use sharp dress and generous coolant |
| Cast iron | Silicon carbide | 46-80 grit, medium hard | Control dust and swarf loading |
| Tungsten carbide | Diamond | 100-220 grit, resin or vitrified | Avoid steel contamination where possible |
⏱ Common Cylindrical Grinding Setups
| Part | Diameter and Length | Starting Feed | Typical Time Driver |
|---|---|---|---|
| Shaft journal finish | 1.5-3 in dia, 3-8 in long | 20-45 in/min traverse | Spark-out and size checking |
| Bearing seat | 25-75 mm dia, 20-80 mm long | 400-900 mm/min traverse | Finish infeed and roundness |
| Long roll cleanup | 4-10 in dia, 12-36 in long | 40-90 in/min traverse | Traverse stroke length |
| Carbide pin | 0.25-1 in dia, 1-4 in long | 4-15 in/min traverse | Light infeed and diamond wheel wear |
💡 Practical Grinding Tips
Grinding a cylinder presents the dilemma of removing metal fast while holding dimensions accurately. Running a grinding wheel at multiple thousands of feet per minute provides a narrow line between those objectives. Sometimes the difference between success and failure is just ten-thousandths of an inch.
Speed and feed matter more then abrasive grains. They’re physical forces that wears out grain and produce heat. They dictate if your part comes out on target…or into the trash.
How to Set Your Machine Correctly
The first setting people typicaly fixate on is the surface speed of the wheel. Most vitrified alumina oxide wheels operates from five thousand to six thousand five hundred surface feet per minute. That’s pretty fast and pushing beyond that rating is counterproductive because centrifugal force can rips the bond away from the abrasive itself. If you are not sure that your machine rpm at the given diameter creates a safe operating speed for your wheel, there is a calculator out there to check it for you. Keep in mind, the new wheel is larger than a worn one, so if you have a worn wheel with the same rpm, it cut slower. Grinding slower than optimal just causes it to be duller and hotter with no benefit added.
The other thing is that workpiece needs to spin much slower than the wheel. Sixty to a hundred surface feet per minute is what you’re looking at on mild steel. As a general rule, more grit points comes into contact with the metal with every wheel turn as the wheel speed goes up relative to work speed. A little too fast and the wheel will skip across the surface, leaving a chaotic spiral; too slow, and the same spots will dig in too deeply, causing a load problem. You don’t want to burn your steel. Because you have hardened tool steels versus soft aluminum, it’s also true that work speed has to be slower to avoid thermal damage on the harder material.
Infeed or feed determines how productive you are. To rough out stock, you want heavy radial cuts, maybe a thou per pass. For finishing, gentle touches is needed, sometimes just two to five ten-thousandths in the last few passes. You need the right traverse feed rate to make sure the wheel is wide enough to cut the material while still leaving enough overlap. Go too fast compared to your wheel width and you end up with uneven cuts. Too slow and you’re creating excess heat as well as grinding away at the exact same surface, tables and tools allow you to see how each variable impacts the other.
The operator can’t wait to get going, so he skips right over step called spark-out. This is an important part of the operation because the wheel removes the last bit of spring-back from the part. If you don’t have sufficient numbers of spark-out stroke, the part will relax and increase slightly beyond the desired size. You might require as many as eight or ten additional strokes (without removing any more metal) for tight tolerance applications. It may seem pointless to spend time without removing any metal, but skipping this step means your part will not be the right size.
As with all machines, setting up the machine variables correctly is crucial. The type of abrasive used is also important. For brittle materials like non-ferrous metals and even cast iron then silicon carbide is an excellent option as it remains sharper for longer on these types of materials. Steels are typically ground using aluminum oxide. Diamond or CBN wheels are required for carbides and other hardened materials, otherwise they will just glaze over.
The other critical factor is coolant. It removes swarf and carries heat away to keep the process stable. So grinding is more about keeping materials off, heat out and vibration down at high speed.
The calculation gives you a starting point, and then your intuition confirms what you should of do. Look for spark color and hear the change in pitch when the wheel bites into the material. Then adjust your feed until it feels right. After setting those values properly, the machine does the rest, and you get finish you need.