Chip Load Calculator for Steel
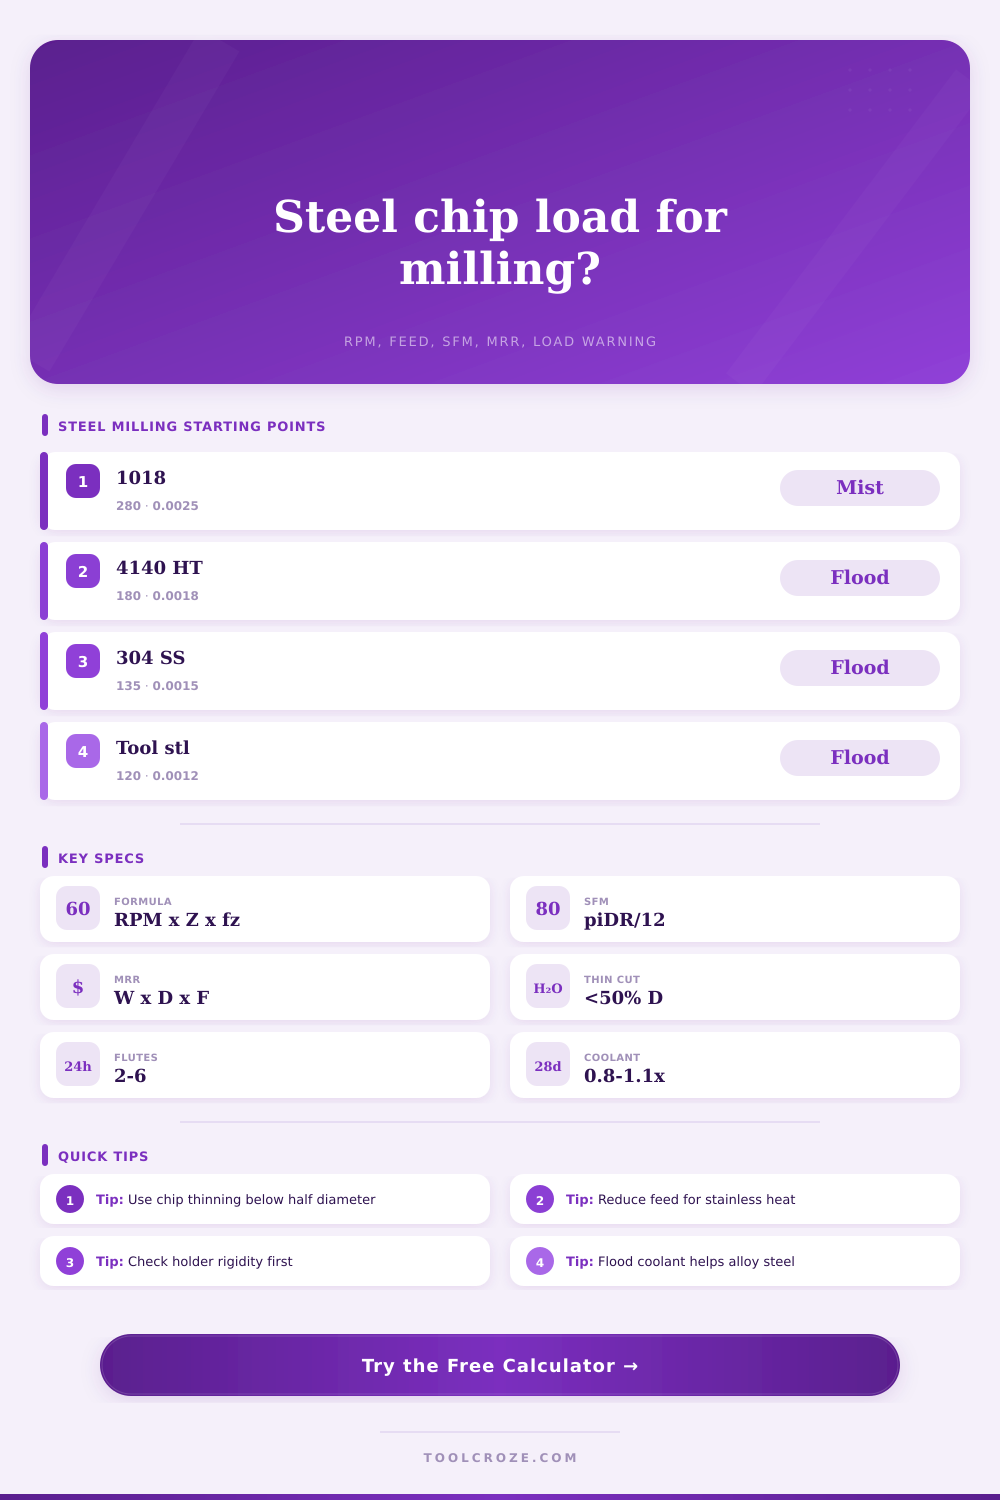
Set steel milling chip load, RPM or SFM, feed IPM, radial chip thinning, coolant factor, MRR, and tool load warning from one cutter setup.
⚙Steel Milling Presets
📐Inputs
Steel Milling Results
🧱Selected Steel and Cutter Grid
🔧Steel Grade Reference
| Steel grade | Typical hardness | Carbide SFM range | Starting chip load | Machining note |
|---|---|---|---|---|
| 12L14 free machining | 110-170 HB | 300-500 SFM | 0.0030-0.0060 in/tooth | Lead improves chip breaking |
| A36 mild steel | 120-180 HB | 240-380 SFM | 0.0020-0.0045 in/tooth | Watch scale and interrupted edges |
| 1018 low carbon | 120-170 HB | 220-340 SFM | 0.0020-0.0040 in/tooth | Good baseline for carbide end mills |
| 1045 medium carbon | 170-220 HB | 190-300 SFM | 0.0018-0.0035 in/tooth | Needs more torque than mild steel |
| 4140 annealed | 190-240 HB | 170-260 SFM | 0.0015-0.0032 in/tooth | Use rigid holding and coolant |
| 4140 heat treated | 280-340 HB | 130-210 SFM | 0.0012-0.0025 in/tooth | Lower SFM and avoid rubbing |
| 304 stainless | 160-220 HB | 100-170 SFM | 0.0010-0.0025 in/tooth | Keep feed positive to avoid work hardening |
| 316 stainless | 150-220 HB | 90-150 SFM | 0.0009-0.0022 in/tooth | More heat sensitive than 304 |
📊Chip Thinning and Engagement Table
| Radial engagement | Factor to programmed fz | Best use | Steel caution |
|---|---|---|---|
| 5% of diameter | 2.29x | Adaptive clearing | Check runout on small tools |
| 10% of diameter | 1.67x | Light radial roughing | Needs enough RPM and coolant |
| 20% of diameter | 1.25x | Productive side milling | Good balance for alloy steel |
| 50% of diameter | 1.00x | Half-slot or shoulder | No chip thinning boost |
| 100% of diameter | 1.00x | Full slotting | Reduce depth or chip load |
🛠Cutter Selection Grid for Steel
| Cutter | Flutes | Diameter range | Steel use | Feed note |
|---|---|---|---|---|
| Carbide end mill | 4 | 1/8-3/4 in | General steel milling | Use table chip load as baseline |
| Variable helix carbide | 5 | 1/4-3/4 in | Alloy and stainless | Often tolerates higher feed |
| Roughing end mill | 4-5 | 3/8-1 in | Heavy roughing | Chipbreaker lowers cutting force |
| HSS end mill | 2-4 | 1/8-1 in | Manual mill and low RPM | Use lower SFM and modest feed |
| Indexable shell mill | 4-8 | 1.5-4 in | Facing and roughing | Check insert chip load range |
🧮Formula Breakdown
| Calculation | Formula | Imperial output | Metric output |
|---|---|---|---|
| Surface speed | SFM = pi x D x RPM / 12 | ft/min | m/min after conversion |
| Feed rate | Feed = RPM x flutes x chip load | IPM | mm/min |
| MRR | MRR = radial x axial x feed | in³/min | cm³/min |
| Chip thinning | Factor = 1 / sqrt(ae/D x (2 - ae/D)) | Multiplier | Multiplier |
| Cut time | Time = length / feed | minutes | minutes |
💡Steel Milling Tips
When a carbide end mill rubs steel at an improper speed, there’s a certain sound. It is a high pitched squeal which typically indicate a lack of cut and more of a rub. Instead of the chip being a crisp curl it becomes a blue, burnt ribbon. Tool life drop to near zero in a matter of seconds.
Steel isn’t about getting to some magic number; it’s about balancing mechanical load with heat and getting the cutter working, not melting. Typically folks begin with a number of feet per minute on surface, and that number depend somewhat on what kind of steel you’re cutting. Hardened alloys require much greater care. Stainless requires it too. But mild steels such as A36 or 1018 can stand up to higher speed.
How to Mill Steel Properly
The calculator does the calculation for you. It takes the rough rules of thumb (surface speed) and turns them into RPMs (revolutions per minute). These RPMs takes into account diameter of your specific tool. Remember, a two inch cutter won’t spin at the same speed as a half inch cutter in order to get the same amount of material removed from the surface. Guessing without the diameter is just that, guessing.
The problem begins here: Feed rate. You must remove a sufficient amount of material per tooth while also shearing steel cleanly. With too little feed, the tool grind on edge of metal. This causes extreme heat buildup and works hardening of the material. This is especially critical with stainless steel. Stainless steel loves work hardening. It’ll wreak havoc on a slow moving or dull cutter in no time flat.
The trick here is that the cutter determine how fast to move based off your spindle speed, number of flutes, and desired chip load. Sounds easy until you’re doing light side cuts. If your radial engagement is less than half of the cutter diameter, what will happen? Even if your programmed feed remains unchanged, the chip becomes thinner. This phenomenon is called chip thinning and it will kill your productivity. You’re thinking you’re cutting with a safe chip load, but in reality, the chip is microscopic. More rubbing occurs which result in premature wear.
Here’s where the software kicks in: It automatically corrects for this. It adds a correction factor to increase the needed feed rate so that the chip remains thick enough to cut cleanly. It is a small detail, but it make all the difference for tool life.
You also need to consider the machine itself. A beefy vertical machining center can runs those aggressive parameters without issue, but a lightweight hobby mill will be rattled to bits. This calculator gives you the option of considering your machine rigidity as well as stickout on tools and whether you are using coolant or not. High pressure mist or even straight flood will push things out just a bit further. It helps not only with chip removal but also with removing heat from the tool. Long tool holders and dry air blasts requires a more conservative approach. This is to avoid deflection and chatter.
On that page there’s a reference table that lays out starting points for all those different steel grades. It provides a starting point for the speed and hardness. But it doesn’t factor in a slight bend in the work piece or a spindle that has seen better days.
The calculator is your place to start with your parameters, but listen to the machine as well. A good cut will sound like a smooth steady roar. A bad one sounds more like a choppy stutter or just plain whine. Reduce the radial depth of cut before dropping the feed rate if you’re hearing the latter. It is often better to keep the chip thick then to slow the feed rate. You risk burning the edge.
All-in-all, milling steel comes down to engagement, speed and feed. You need enough engagement while removing material fast but not too fast as to burn up the tool. By knowing how each of these factors relate to one another, you go from guessing to controlling milling steel. It’s all about getting clean chips, cool tools and smooth surfaces. So don’t let it hit that high pitch squeal, and typically everything else will fall in line.