SFM to SMM Calculator
Convert surface feet per minute to surface meters per minute, calculate RPM from tool diameter, compare the result with material speed ranges, and apply a safety derating factor.
📌Material and Tool Presets
⚙SFM, SMM, Diameter, and RPM Inputs
SFM to SMM Results
Full Breakdown
🧱Material Speed Grid
📊SFM to SMM Conversion Table
| SFM | SMM / m/min | 1/2 in Tool RPM | 12 mm Tool RPM |
|---|---|---|---|
| 100 SFM | 30.5 m/min | 764 RPM | 809 RPM |
| 250 SFM | 76.2 m/min | 1,910 RPM | 2,021 RPM |
| 500 SFM | 152.4 m/min | 3,820 RPM | 4,042 RPM |
| 800 SFM | 243.8 m/min | 6,112 RPM | 6,468 RPM |
| 1,200 SFM | 365.8 m/min | 9,167 RPM | 9,702 RPM |
🔧Material Speed Reference
| Material | Typical Carbide SFM | Equivalent SMM | Starting Note |
|---|---|---|---|
| 6061 aluminum | 600 to 1,200 | 183 to 366 | Use chip evacuation and avoid rubbing built-up edge. |
| Mild steel 1018 / A36 | 250 to 450 | 76 to 137 | Stable setup and coolant allow the upper half. |
| 304 stainless steel | 120 to 220 | 37 to 67 | Stay fed; work hardening punishes rubbing. |
| Titanium Ti-6Al-4V | 80 to 140 | 24 to 43 | Heat control and engagement matter more than peak RPM. |
| Gray cast iron | 250 to 450 | 76 to 137 | Dry cutting is common; control dust and edge wear. |
| Inconel 718 | 50 to 90 | 15 to 27 | Use conservative speed and rigid workholding. |
⚒Tool and Operation Adjustment Table
| Setup Choice | Speed Factor | Feed Effect | Use When |
|---|---|---|---|
| High speed steel | 0.35x | Lower heat tolerance | Manual mills, drills, reamers, or low-cost tooling. |
| Coated carbide | 1.15x | Can hold heat better | Stable holders, good coolant, coated end mills or inserts. |
| Full slotting | 0.70x | Higher engagement | Tool is buried near full diameter in the cut. |
| Face milling | 1.05x | Often smoother chip | Multiple inserts, shallow depth, consistent engagement. |
| Manual feed | 0.80x | More reserve | Handwheels, light machines, uncertain rigidity, or chatter risk. |
📏Diameter and RPM Quick Grid
| Tool Diameter | 100 SFM | 300 SFM | 800 SFM | 1,200 SFM |
|---|---|---|---|---|
| 1/8 in / 3.18 mm | 3,056 RPM | 9,167 RPM | 24,446 RPM | 36,669 RPM |
| 1/4 in / 6.35 mm | 1,528 RPM | 4,584 RPM | 12,223 RPM | 18,335 RPM |
| 1/2 in / 12.7 mm | 764 RPM | 2,292 RPM | 6,112 RPM | 9,167 RPM |
| 1 in / 25.4 mm | 382 RPM | 1,146 RPM | 3,056 RPM | 4,584 RPM |
| 3 in / 76.2 mm | 127 RPM | 382 RPM | 1,019 RPM | 1,528 RPM |
💡Speed Calculation Tips
Speed makes all of the difference between a sharp tool and a destroyed one. Yes, you might own the worlds best carbide end mill but if you run it too quickly for the material, you’ll burn the edge off without taking a single meaningful cut. Run it too slowly and you’ll rub the work piece, creating enough heat to blunt the cutting edge far quicker then any impact ever would.
And this is where surface speed beats spindle speed; the former does the math after you input your diameter and material, saving you from having to guess at conversions and numbers. It removes feet/meter confusion so you can concentrate on actualy making the cut.
Why Speed Matters for Your Tools
In the West, many shop use SFM (surface feet per minute) as their standard for a machining operation. It shows how quickly the cutting edge move over the materials surface. In SI units, this would be SMM: Surface Meters Per Minute. Multiplying by zero point three zero four eight converts SFM to SMM.
What throws people off though is understanding the concept of SFM. When you think about it, a 1/2 inch drill bit at a given RPM is quite different from a one inch diameter drill bit at the same RPM. Obviously, the former will cover less ground with each revolution. And that’s where many folks gets confused. On machine dial, they see the RPM number and assume they’re set. What they don’t realize is that changing the tool size change the actual speed at which it’s working on the piece.
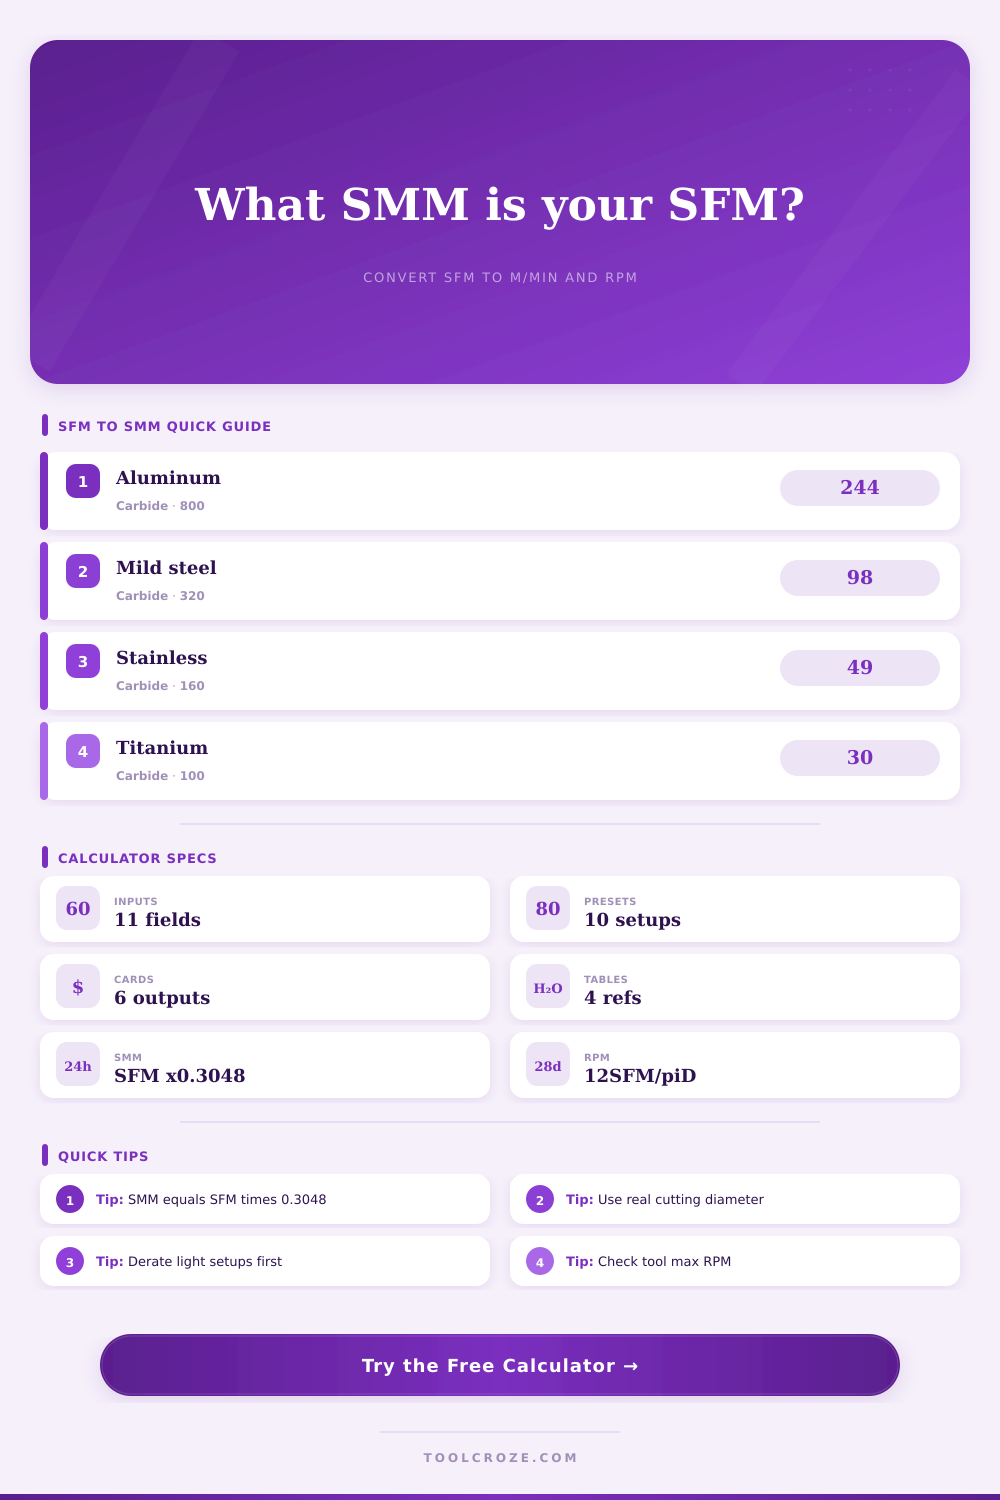
The starting point is material you are cutting. Aluminum runs fast, typically between six hundred and twelve hundred SFM with carbide tools. Because it doesn’t work-harden aggressively, aluminum also dissipates heat well so you can push it pretty hard.
Not so with steel. Mild steel will commonly run in the two hundred to four hundred SFM range. Stainless steel is worse yet; you frequently need less than two hundred SFM before you start working-hardening the material. Titanium is famously fussy, requiring both high rigidity and low speeds. This gets laid out in the reference table on the page, where you see that lower speeds are needed as materials becomes more heat-sensitive or tough.
It’s not about matching the tool to the machine; it’s about matching the tool to the material. The charts are just that, they get you started. Ideal lab conditions don’t translate into real world condition very well.
Enter the concept of derating. Need to run a light set up? You can slot out a deep pocket. Slow things down. You can add a safety factor in the calculator that will decrease the suggested speeds by as much as 10%, 20% or even 30%. That may sound conservative, but it’s practical. Dropping your speed by 10% may mean losing a minute on a five minute job but doubling the life of your tool. Saving a few minutes by rushing a cut often result in broken tools and having to restart the job, costing you far more time then you saved.
How fast you can actually go depends largely off coolant and rigidity. The chart numbers are generally more accurate with flood coolant because it removes heat from the cutting area. Mist cooling or dry machining require care. Longer, slender holders mean less rigidity, so slow the speed down to prevent chatter. Chatter tears up tool edges and screws up the surface finish.
A high pitched scream, chatter means there’s something wrong. Adding more RPM won’t help. You usually should of lighten the load or slow down.
This relates to feed rate. With the RPM now considered safe, if you know how many flutes your cutter has and want to run with some specific chip load, you multiply those together and then multiply them by your RPM to arrive at your feed rate (inches per minute). For you, the calculator figures that out and presents the full picture. It shows you what the raw chart RPM should be and then lowers it to the recommended RPM; it also shows the effective speed you are actualy running at based on your spindle settings.
If you’re only able to run at less than the suggested RPM due to limitations of the machine, then you will be running slower then the tool anticipates. You’ll likely have to adjust the feed to make up for this or just accept that cycle time will increase.
It’s all about balance Maintain balance. Speed This is a tool for removing metal efficiently while preserving both parts and tools. Pulling on that lever gets you balanced. Think of the numbers as a guide, not a rule. Listen to the machine, watch the chips. Blue ones = you’re too hot. Shiny, curly ones = you’re probably in the sweet spot. Get close with the numbers, but let your ears and eyes tell you when you’ve got it right. Go conservative at first then push it. That’s how you learn what your setup can realy do.