Drilling Feed Rate Calculator Metric
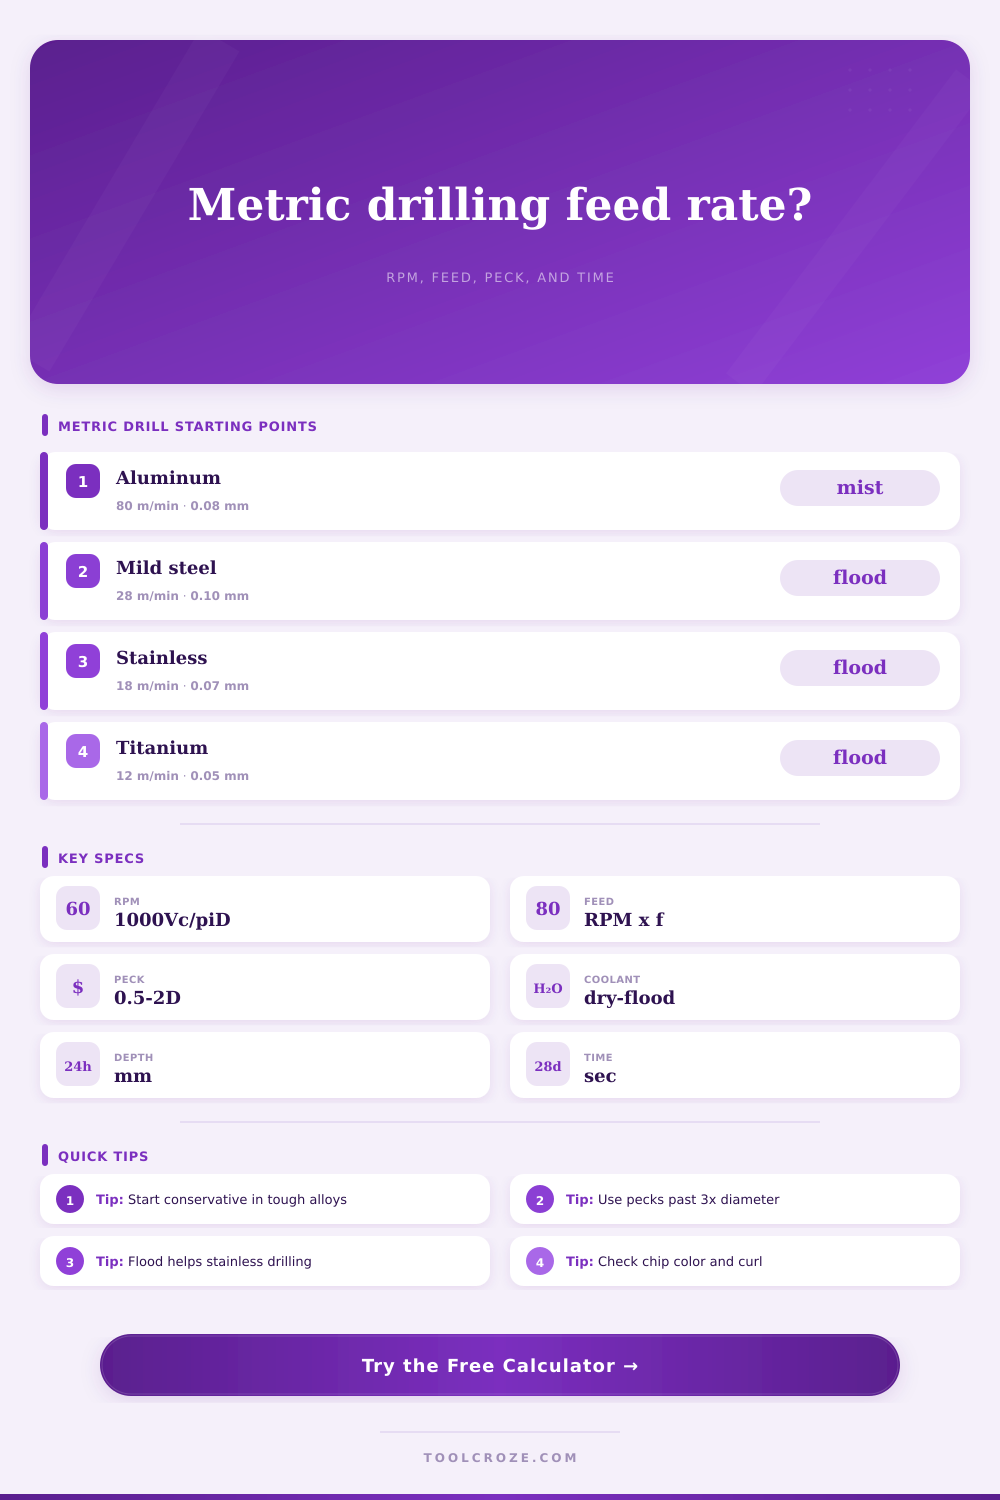
Calculate metric drill RPM, feed in mm/min, peck depth, hole cycle time, coolant adjustment, and material-specific starting points.
⚙Metric drill presets
🔩Drill and material inputs
Use the actual drill diameter, not the tapped thread size.
Calculator applies coolant factor to this starting speed.
For twist drills, feed per rev is the main feed input.
Enter a machine spindle speed if you cannot run the calculated RPM.
Cycle time includes feed travel, breakthrough allowance, peck retract allowance, and a short approach time per hole. It does not include tool changes, clamping, probing, or operator handling time.
📊Drill and material grid
📘Metric speed and feed reference
| Material | Starting Vc m/min | Feed for 3-6 mm | Feed for 6-12 mm | Coolant note |
|---|---|---|---|---|
| Aluminum 6061 / 6082 | 70-100 | 0.04-0.08 mm/rev | 0.08-0.18 mm/rev | Mist, flood, or air blast |
| Mild steel | 22-32 | 0.04-0.08 mm/rev | 0.08-0.16 mm/rev | Oil or flood coolant |
| Stainless steel 304 / 316 | 12-22 | 0.03-0.06 mm/rev | 0.06-0.12 mm/rev | Flood coolant preferred |
| Cast iron | 18-30 | 0.04-0.08 mm/rev | 0.08-0.18 mm/rev | Dry or air, control dust |
| Brass / bronze | 55-85 | 0.04-0.10 mm/rev | 0.10-0.22 mm/rev | Light oil if needed |
| Titanium alloy | 8-16 | 0.02-0.05 mm/rev | 0.05-0.10 mm/rev | Strong flood coolant |
| Acrylic / polycarbonate | 40-70 | 0.03-0.08 mm/rev | 0.08-0.18 mm/rev | Air blast, avoid heat |
| Hardwood / MDF | 70-120 | 0.05-0.15 mm/rev | 0.15-0.35 mm/rev | Chip extraction |
🔧Common metric drill presets table
| Preset | Diameter | Material | Depth | Starting setting |
|---|---|---|---|---|
| Small brass pilot | 2.0 mm | Brass | 8 mm | High RPM, light feed |
| Acrylic panel hole | 3.0 mm | Acrylic | 5 mm | Clear chips often |
| Titanium lug hole | 4.0 mm | Titanium | 10 mm | Low speed, flood coolant |
| Aluminum plate hole | 5.0 mm | Aluminum | 12 mm | Mist coolant, moderate feed |
| M8 tap drill | 6.8 mm | Mild steel | 18 mm | Peck at about 1D |
| Stainless bracket | 8.0 mm | Stainless | 16 mm | Do not dwell |
| Cast iron clearance | 10.0 mm | Cast iron | 25 mm | Dry, steady feed |
| Deep aluminum bore | 20.0 mm | Aluminum | 60 mm | Wide pecks, chip evacuation |
📝Peck drilling and cycle time guide
| Hole depth ratio | Suggested peck | Retract allowance | When to use |
|---|---|---|---|
| Up to 2D | No peck or 2D | 0-1 sec per peck | Through holes with good chip flow |
| 2D to 4D | 1D to 1.5D | 1-2 sec per peck | General workshop drilling |
| 4D to 6D | 0.5D to 1D | 2-3 sec per peck | Blind holes or stringy chips |
| Over 6D | 0.5D or less | 3+ sec per peck | Deep holes, coolant-starved cuts |
💧Coolant factor table
| Coolant method | Speed factor | Feed confidence | Best fit |
|---|---|---|---|
| Dry / air only | 0.90 | Lower heat margin | Cast iron, wood, light aluminum |
| Mist coolant | 1.00 | Good chip clearing | Aluminum and plastics |
| Flood coolant | 1.10 | Stable temperature | Steel and stainless |
| Through-tool coolant | 1.20 | Best for deep holes | CNC deep drilling |
When a drill is doing its job well, you know it by the smell of hot metal and cutting fluid. That means you’re getting somewhere.
If you spin it too fast or let it sit in one place for to long, you’ll know it by a different smell: the sharp, acrid odor of burning steel. Even though it only has one axis of motion, drilling can be an unforgiving process. Get the feed rate wrong and you may burn the workpiece; you may break the drill; you may make a hole that’s too wide.
How to Drill Safely and Well
The metric drilling feed rate calculator does those math problem for you. It turns abstract charts into exact spindle speed and feed rates suitable for your machine.
Drilling presents a problem: How do you balance speed against material removal? To answer that, there are two factors. One is cutting speed, how rapidly does the drill turn on its edge? The second is the feed rate, how far does the tool advance per turn?
You can go too slow or too fast, and both will result in a rubbed-out drill bit rather than a cut. Rubbing creates tons of heat and makes the metal (stainless steel in particular) harder, so it’s virtually impossible to drill through.
Flood coolant is important for keeping cutting edge stable at a good temperature. Not only does it wash away the chips, but it also ensures the metal stay soft and shears off cleanly.
Cutting Speeds: Cutting speeds are based off the speed recommendations from the machine manufacturers. It is assumed that they is using new drills in a rigid machine tool. In the real world, things aren’t so rosy.
That’s where the machine rigidity factor comes into play on the calculator. If you have a light-weight mill, or a good old bench drill press, then you can’t approach it like you would a big beefy CNC center. The hole will wander, the tool will deflect, and the drill bit will snap off.
By lowering your rigidity factor you’ll decrease the recommended speeds and give yourself a safe margin of error. It is not much, just enough to save you some set-up frustration and more expensive furnitures.
You may also have heard of peck drilling. This also can be confusing, particulary if you’ve been doing clearance holes in wood and are now operating deeper. As a drill plunges deeper, the flutes fills up with chips. When these chips don’t get out, they jam up and become sort of a grinding abrasive paste between the drill bit and the material being cut. Friction rises dramatically; so does heat.
With each peck, the drill backs off for a moment, breaking the chips and letting coolant flush across the cutting edge. How deep you go determines how many pecks will be required; the peck factor dictates this. So even though it might feel like pecking slows you down, it prevents bog-down and maintains a consistent average feed rate.
The whole equation becomes different than what materials you use. For example, aluminum cuts fast and is forgiving. All you need is air or maybe a little mist coolant to knock out those sticky chips.
Titanium is like a thermal battery. You realy have to go slow and steady, cutting it with lots of coolant. If that drill heats up, you won’t make it through a single hole.
The starting points come from the reference tables on the page. But these are only starting points. The actual art comes into play when you listen to the machine.
If it’s humming smoothly and low then you’re dialed in. If there’s a stutter on the feed, or it sounds like a high pitched squeal, then you’re probably spinning too fast for the material or not feeding it enough.
Look at the chips. Your eyes and ears will tell you more than any calculator ever could. For example, good chips is continuous ribbons for aluminum; they’re blue-ish and curly for steel. Bad ones are welded to the flute, dark, or powdery.
Dial it in by using your eyes and ears while getting close with the numbers. Go conservative if cutting a deep hole or a tough alloy. When the process settles, step up the speed or feed to increase your material removal rate.
You should of balance tool life and efficiency. That is what separates a rough draft from a finished part.