Thread Feed Rate Calculator
Calculate synchronized feed per revolution, feed rate, thread travel, spindle revolutions, and pass-based cycle time for lathe threading, tapping, and thread milling.
📌Threading Presets
⚙Thread Feed Inputs
Thread Feed Rate Results
🧵Thread Spec Grid
📊Metric Thread Feed Reference
| Thread | Pitch | Feed per rev | Feed at 400 RPM |
|---|---|---|---|
| M3 x 0.5 | 0.50 mm | 0.50 mm/rev | 200 mm/min |
| M5 x 0.8 | 0.80 mm | 0.80 mm/rev | 320 mm/min |
| M6 x 1.0 | 1.00 mm | 1.00 mm/rev | 400 mm/min |
| M8 x 1.25 | 1.25 mm | 1.25 mm/rev | 500 mm/min |
| M10 x 1.5 | 1.50 mm | 1.50 mm/rev | 600 mm/min |
| M12 x 1.75 | 1.75 mm | 1.75 mm/rev | 700 mm/min |
| M16 x 2.0 | 2.00 mm | 2.00 mm/rev | 800 mm/min |
| M20 x 2.5 | 2.50 mm | 2.50 mm/rev | 1000 mm/min |
📏Imperial TPI Feed Reference
| Thread | TPI | Feed per rev | Feed at 300 RPM |
|---|---|---|---|
| #10-24 | 24 | 0.0417 in/rev | 12.5 in/min |
| 1/4-20 | 20 | 0.0500 in/rev | 15.0 in/min |
| 5/16-18 | 18 | 0.0556 in/rev | 16.7 in/min |
| 3/8-16 | 16 | 0.0625 in/rev | 18.8 in/min |
| 7/16-14 | 14 | 0.0714 in/rev | 21.4 in/min |
| 1/2-13 | 13 | 0.0769 in/rev | 23.1 in/min |
| 5/8-11 | 11 | 0.0909 in/rev | 27.3 in/min |
| 3/4-10 | 10 | 0.1000 in/rev | 30.0 in/min |
🔧Threading Operation Reference
| Operation | Main feed formula | Pass count use | Important input |
|---|---|---|---|
| Lathe external | RPM x thread lead | Multiple depth passes plus spring pass | Pullout or relief distance |
| Lathe internal | RPM x thread lead | Often slower retract and checking | Bore clearance and overrun |
| Rigid tapping | RPM x pitch or lead | Usually one feed-in pass | Exact spindle synchronization |
| Floating tapping | RPM x pitch or lead | One pass with holder float allowance | Compression and tension travel |
| Internal thread mill | Helical path feed from programmed feed | Often one or more helical passes | Hole diameter and cutter diameter |
| External thread mill | Helical path feed from programmed feed | Rough and finish radial passes | Major diameter and cutter diameter |
🗂Preset Scenario Reference
| Preset | Operation | Thread spec | Typical planning check |
|---|---|---|---|
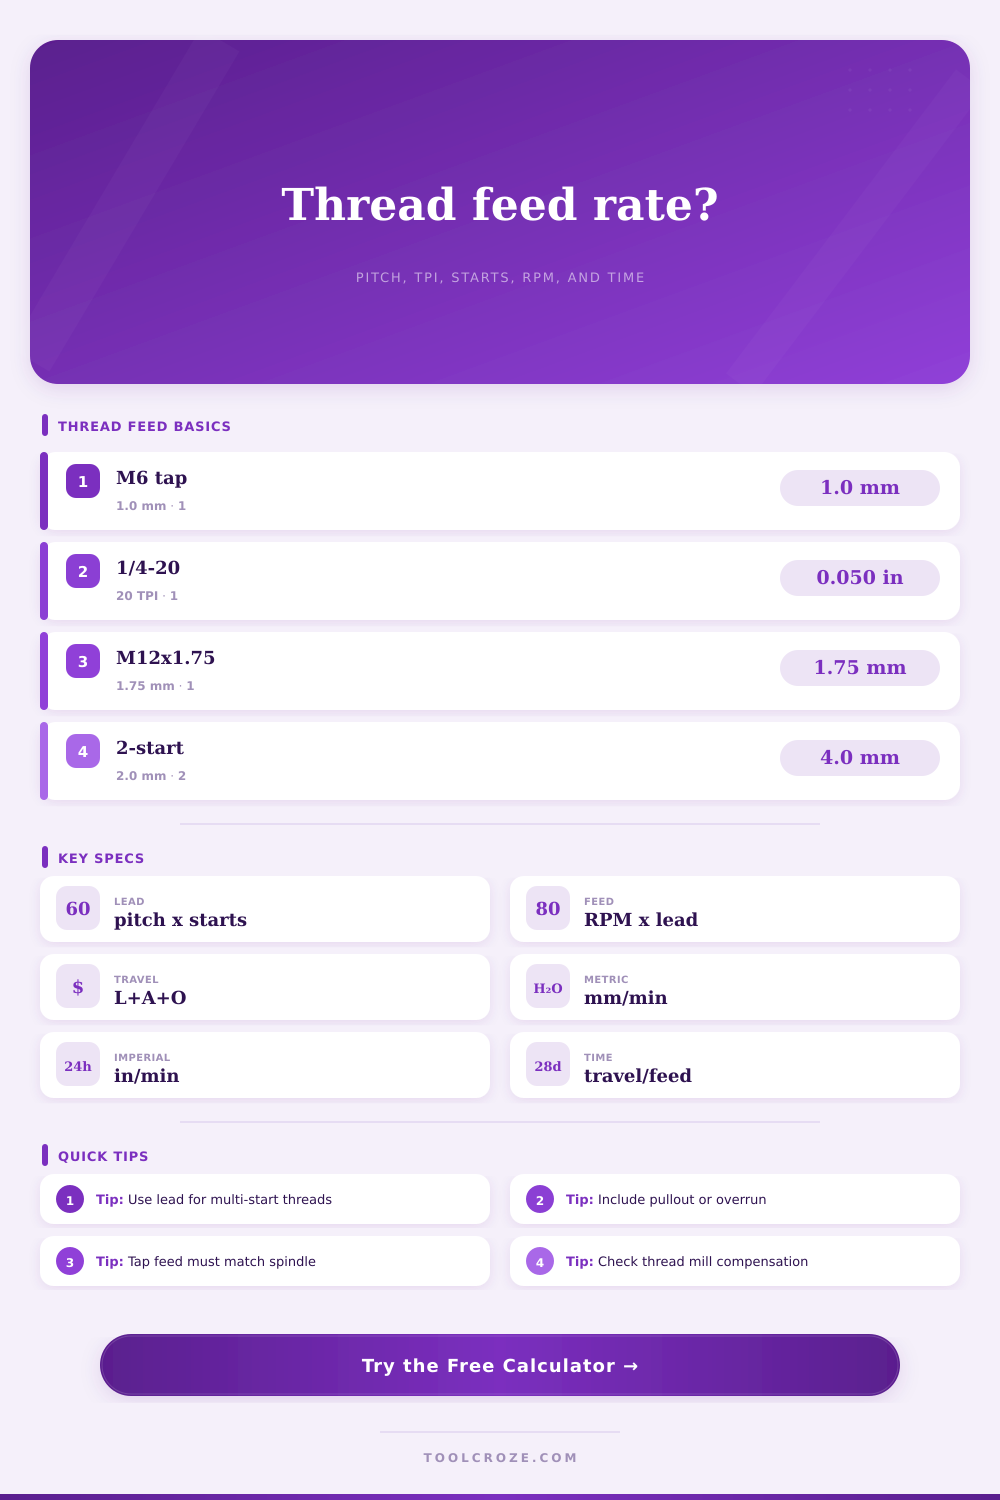
| M6 x 1 Tap | Rigid tapping | 1.00 mm pitch, 1 start | Tap feed and depth time |
| 1/4-20 Tap | Floating tapping | 20 TPI, 1 start | Feed in inches per minute |
| M12 x 1.75 Lathe | External lathe | 1.75 mm pitch, 1 start | Pass count cycle time |
| M20 Two-Start | External lathe | 2.50 mm pitch, 2 starts | Lead versus pitch check |
| M10 Thread Mill | Internal thread mill | 1.50 mm pitch, 1 start | Centerline feed adjustment |
💡Calculation Tips
If you’ve ever had a tap break off in a newly drilled hole, you know what I’m talking about. If an operator doesn’t understand how cutting tool relates to spindle rotation, this will happen. When he stop feeding the tool forward, the spindle continues turning and will either shear the cutter or strip threads out of the workpiece.
To survive, you must be able to calculate thread feed rate. The calculator above do it for you. Knowing what those numbers mean saves your cutters.
How to Stop Taps from Breaking
So that leads us back to the heart of all this: lead. Lead is length the tool travels for each full rotation of the spindle. Lead on a normal thread (single start) is identical to pitch. So if I’m cutting an M10 thread with a 1.5 millimeter pitch, then with each complete turn of the chuck the tool need to move exactly 1.5 millimeters. That’s rigidly synchronized. Move the tool too far and threads get cross cut and ruined. Move it too short and tap binds.
In rigid tapping there has to be rock solid coordination between axis and motor, because machine knows the pitch and locks down the motion to the rotation. Things get much more complicated with multi-start threads. These threads have multiple helical paths and they runs parallel to one another. For example, a two-start thread would have twice as much lead than the pitch. So if your pitch is 2.0 millimeters then you need to advance tool 4.0 millimeters every revolution.
This is where things can get tricky. Sometimes people enter the pitch value into their feed rate command without considering how many starts there are. They end up setting a feed rate equal to half of actual lead. This leads to vibration, dragging, or worse, a broken tool. The calculator will do this math for you, making sure you’re feeding at the proper lead versus just raw pitch value.
That lead turns into a linear feed rate, which is shown in inches or millimeters per minute, based off the spindle speed. A linear feed rate of 600 millimeters per minute means if your spindle spins at 400 RPM and you have 1.5 millimeter lead, then every second tool will advance 600 millimeters. That number give an idea about the rate the tool travels through material. It also tells you whether machine can physically keep up with demand. It also helps you estimate cycle time.
Because high-speed threading demands rapid acceleration and deceleration of servo motors, it stress the drive system. There is another issue with synchronizing taps: the tapping itself. There are two types: rigid and floating.
Rigid uses electronic control of feed rate in machine to sync with speed of the spindle. Floating tapping relies on mechanical flexibility in holder so that tap feeds according to the shape of what it’s cutting (i.e., how fast a given tap cuts into material). In floating tapping, the holder provides mechanical compliance to let tap feed at its own rate, but there’s still feed rate control on your machine; it’s just a more forgiving range within which it needs to be set.
But unless you have proper feed, you’ll either overload the machine or thing being tapped. That’s where table on the page comes into play, laying all that out for typical sizes so you can quickly check yourself before you cut anything.
Don’t forget cycle time when you’re first planning. Depth of hole isn’t all there is to cutting a thread. There’s pullout/overrun distance; there’s approach distance and then the thread length itself. How much room do you have for clearance on the thread tap as it backs out of the hole? How far away from hole does the lathe tool has to be so that it engages fully to cut the thread profile? Failing to allow for those times can result in broken taps at the exit point or an incomplete thread. A few seconds of added index and retract time between each pass can make big difference in how fast you produce.
In another option known as thread milling, the cutter turns around while following a helical path. The feed is determined by the thread pitch and cutter diameter. Because it’s programmed as a continuous cut, this method isn’t quite as vulnerable to spindle synchronization errors. But you need to be mindful of relationship between hole diameter and cutter size, the bigger the cutter, the quicker it can do the work, but it might be too large for the hole.
Which process you use (thread milling or tapping) depends mostly on how accurate thread needs to be, as well as material hardness. But ultimately, it comes down to understanding the geometry. Thread forms are exact mathematical curves. Your machine need to reproduce them faithfully. And whether you’re tapping a hole or milling a thread or turning one on a single-point lathe tool, this applies.
The tool should of always be fed at the exact rate determined by the thread lead. It’s a tiny little thing but it makes all the difference. When you understand that tool needs to synch with the spindle rotation, you don’t guess anymore; instead, you cut confidently because the tool moves, the spindle spins, and the thread gets made correctly.