Wire EDM Feed Rate Calculator
Estimate linear feed, cut time, kerf width, taper spread, and effective area rate from material, thickness, wire diameter, spark gap, pass type, and cut length.
⚙ EDM Presets
📏 Cut Inputs
Wire EDM Feed Estimate
🧮 Material & Wire Snapshot
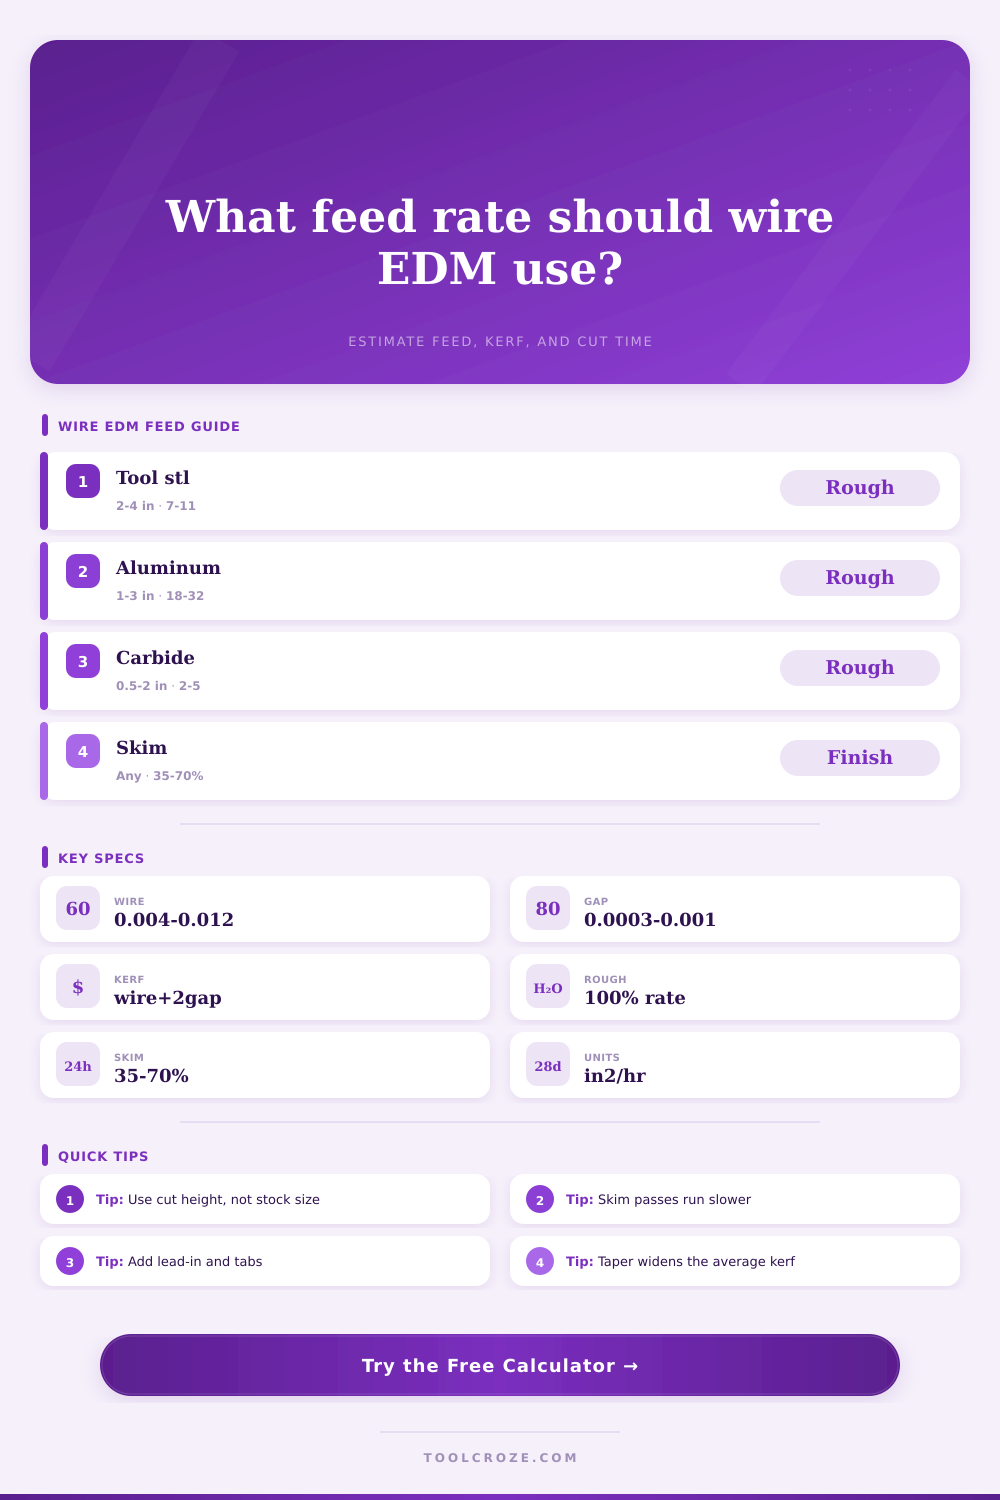
📊 Material Cutting Reference
| Material | Typical Rough Rate | Relative Factor | Notes |
|---|---|---|---|
| Tool steel / D2 / A2 | 7 to 11 in²/hr | 1.00 | Baseline hardened die work |
| Mild steel | 10 to 16 in²/hr | 1.25 | Stable flushing, moderate speed |
| Stainless steel | 6 to 10 in²/hr | 0.88 | Heat and flushing sensitive |
| Aluminum | 18 to 32 in²/hr | 2.35 | Fast, but watch wire vibration |
| Copper / brass stock | 8 to 14 in²/hr | 1.15 | Conductive but can load settings |
| Titanium | 4 to 8 in²/hr | 0.68 | Use conservative flushing |
| Tungsten carbide | 2 to 5 in²/hr | 0.38 | Slowest profile group |
| Inconel / nickel alloy | 3 to 7 in²/hr | 0.55 | High heat, slower servo response |
🔧 Wire Diameter & Kerf Guide
| Wire Diameter | Common Use | Typical Gap/Side | Approx Kerf |
|---|---|---|---|
| 0.004 in / 0.10 mm | Fine ribs, micro details | 0.0002 to 0.0004 in | 0.0044 to 0.0048 in |
| 0.006 in / 0.15 mm | Small punches, thin forms | 0.0003 to 0.0005 in | 0.0066 to 0.0070 in |
| 0.008 in / 0.20 mm | General precision work | 0.0004 to 0.0007 in | 0.0088 to 0.0094 in |
| 0.010 in / 0.25 mm | Standard rough and trim | 0.0005 to 0.0010 in | 0.0110 to 0.0120 in |
| 0.012 in / 0.30 mm | Thick stock roughing | 0.0008 to 0.0013 in | 0.0136 to 0.0146 in |
🎯 Pass Type Multipliers
| Pass Type | Feed Multiplier | Offset Purpose | Finish Intent |
|---|---|---|---|
| Rough cut | 1.00 | Main stock removal | Fastest profile opening |
| First trim | 0.70 | Remove recast and bow | Better straightness |
| Second trim | 0.52 | Refine wall and corner | Fine finish |
| Light skim | 0.38 | Final size correction | Highest accuracy |
📐 Thickness, Taper & Time Examples
| Scenario | Thickness | Cut Length | Typical Result |
|---|---|---|---|
| Thin shim skim | 0.125 in | 8 in | High feed, short time |
| 2 in tool steel | 2.000 in | 16 in | About 2 to 4 hours |
| 4 in die block | 4.000 in | 20 in | Slow feed, long cut |
| 3° taper cavity | 1.500 in | 12 in | Wider average kerf |
💡 Practical EDM Notes
Silence is golden on a good-running wire EDM floor. It is not silent void of unoccupied space. It is the almost inaudible sound of dielectric fluid coursing around, with tiny spits and pops of sparks cutting away metal without touching it. If you have never witnessed a spark machine eating its way through hardened tool steel, it can seem like magic the first time.
That illusion quickly fades under pressure of a tight timeline, or a stubbornly tough-to-machine material change. In that moment, you begin to wonder whether you’re pushing too hard on the feed rate to make the quote or being too easy on it to preserve the part. This calculator does the number crunching for you, but knowing what those digits mean are the difference between a good cut and a scrap bin.
Why Wire EDM Needs More Than Just Speed
Related article: Why Your Tool Steel Is Harder Than Most
On any given program, most shops begins with their area rate, typically expressed in square inches per hour. That all makes sense on paper, until you consider the geometry of the cut. A half-inch profile in two-inch steel removes the same volume of material as a two-inch profile in half-inch steel, yet they behaves completely differently. But these are entirely different animals. Because the cut is thinner, it’s less likely to trap debris; the thicker cut flushes it out better, so you can feed faster without risk of short circuiting. To handle this, the tool ties thickness right into feed speed and total run time. Instead of worrying only about how fast your wire moves along the tube, it makes you think about the volume of debris exiting the kerf.
The type of material does make a big difference. Some will erode very cleanly, and aluminum may have a high rate area in the chart above. However, they tend to load the spark gap rather easily unless you’re really good at keeping it flushed out. Other materials is harder, like tungsten carbide, which is tough to cut as it’s dense and hard to erode. But it produces less waste material that clogs up the cut. This pattern gets reflected in the reference table on the page where the tool steel is set as a base line with other materials varying by hardness and conductivity.
Respect what the material is made of. Ease off too far on the carbide and you burn up the machine’s daily cutting capacity. Too far with aluminum and you ruin the wire.
Many operators treats the rough cut as the only important phase, but the skim passes define the final quality because the rough cut creates a recast layer (a thin skin of re-solidified metal) that is dimensionally incorrect or can lead to micro-cracking. That’s why skimming is necessary; it gets rid of this layer but must be done at slow feed rates and with little power to keep it stable. Running a skim pass at the same speed you used on the rough cut will lead to a poor surface finish or even breakage of your wire. The calculator takes into account these factors with multipliers against the feed rate to remind you that finishing isn’t about just getting stuff off, but also improving what remains.
One other variable causing issues is the Kerf Width, especially with tight tolerances. The kerf is actually larger than the wire diameter. The spark gap is on each side of the wire. That means the gap change as the wire size changes or the power increases or decreases. Then you add a twist for taper and the kerf widens out different depending on height. So if you don’t account for taper and spark gap you’ll have a piece that’s too small for the end. The machine accounts for this by assuming there is a gap (spark gap) and then adding the wire dia to twice that gap. It also takes into account the taper spread. A tiny bit but a thousandth here makes a big difference in precision work.
And don’t overlook the time overhead. Threading and lead-in/out can really add up. That program may appear very efficient on paper, but what if the machine threads ten seconds per inch of wire? Then the clock continues to tick. There are fields in the calculator for machine efficiency and overtravel which recognize that there’s not always a direct correlation between what the machine does theoretically versus what it actualy does. It builds in some overhead time for the interruptions that happen in real life.
Speed isn’t everything with wire EDM. To succeed, you must master the trade-offs between wire life, surface finish, and time. There are numbers. These numbers aren’t arbitrary once you realize what they do together: material, thickness, and pass strategy. The ones that turn into your road map. These numbers brings back the stillness to the shop floor, where you can see exactly how quickly the wire’s ripping, and why.